Structural adhesive
- Make
- Land Rover
- Model
- Range Rover L322 Range Rover Service Procedures
- Section
- STRUCTURAL SEALING › Structural adhesive
CORROSION PREVENTION AND SEALING
-4
STRUCTURAL SEALING
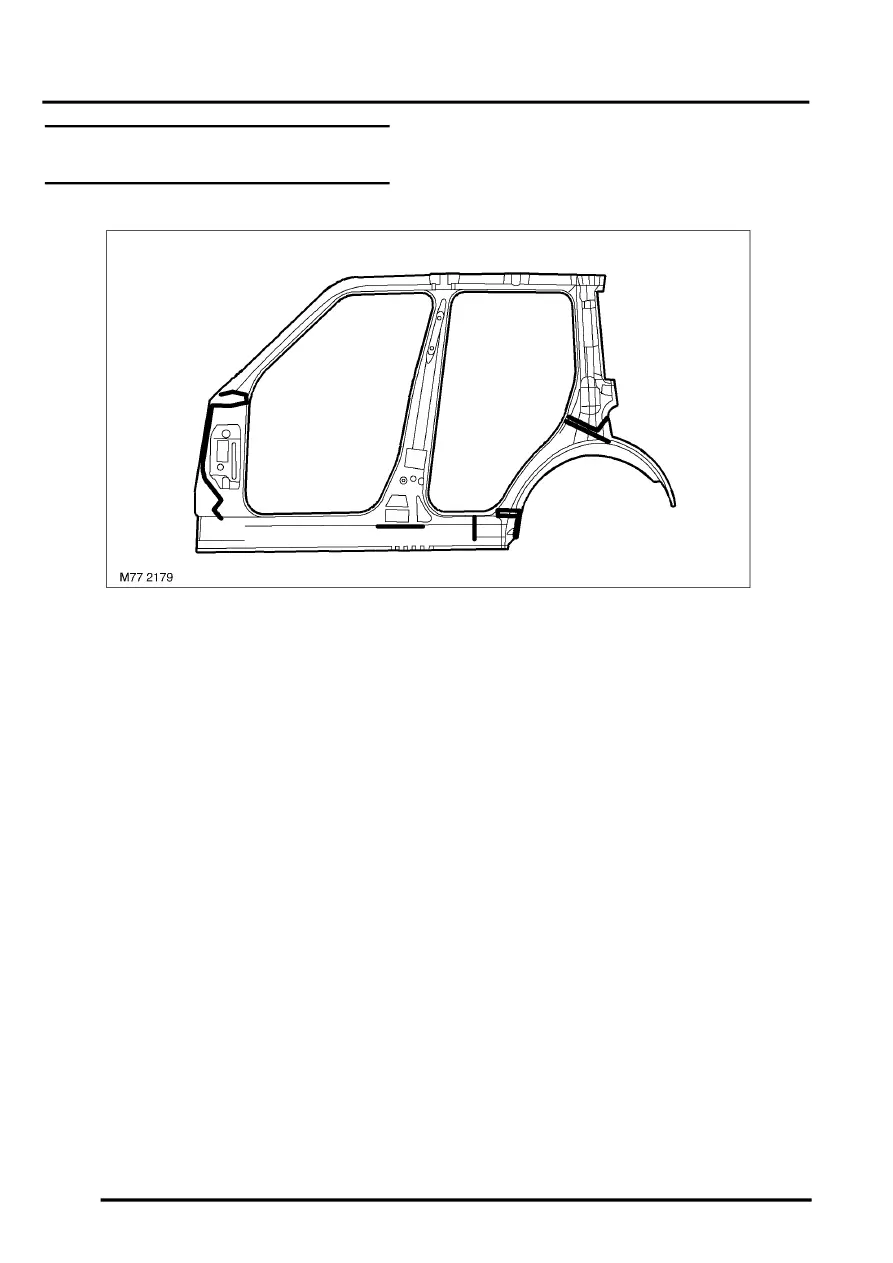
Structural adhesive on body side frame -
inner
Joints symmetrically opposite to those shown are also treated. Apply 3 mm diameter beads to all joints shown. Leave
sill drain points free of adhesive.
Structural adhesive
Metal-to-metal adhesive is applied to critical joint areas during factory assembly. The material used is a high-
temperature, heat cured, nitrile phenolic which serves to bond two metal surfaces and also to seal the joint against
ingress of dust, moisture and fumes. This material is not suitable for service use and, during repair, should be
substituted by an approved Structural Adhesive.
Those joints which require the application of structural adhesive are detailed in the previous illustrations. Only joints
applicable to service panels are included. Apply structural adhesive where indicated or to the mating panel surface.
CAUTION: When separating a joint treated with metal-to-metal adhesive, it is important to avoid distortion.
Heat the joint gradually until the bond weakens sufficiently to permit panel separation.
NOTE: When spot welding through metal-to-metal adhesive, take particular care to adjust the transformer setting to
ensure a reliable weld.
Parts & tools for this job For Land Rover Range Rover
- TOOLTorque wrenchSearch: 3/8 inch torque wrench
- TOOLSocket setSearch: socket set metric
- BOOKHaynes manualSearch: Haynes manual Land Rover Range Rover
Links open Amazon search results in a new tab. As an Amazon Associate I earn from qualifying purchases.