Zinc-plated Steel Repair
- Make
- Rover
- Model
- 400 Body Repair Manual
- Year
- 1995–2000
- Section
- Body repairs › Zinc-plated Steel Repair
Zinc-plated Steel Repair
The zinc-plated steel used in some panels of the vehicle requires different repair techniques than for ordinary mild steel.
Refer to "Construction" for the location of the zinc-plated panels.
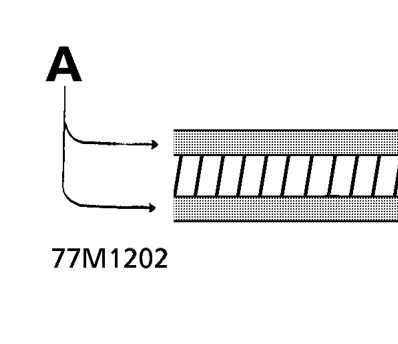
A Zinc Plating (5-6 microns) B Steel plate
- Before spot welding the zinc-plated steel, remove the paint from both sides of the flange to be welded. Apply sealer to the flange after welding.
NOTE: Seal the sanded surfaces thoroughly to prevent rust.
WARNING: To prevent eye injury, wear goggles or safety glasses whenever sanding, cutting or grinding.
- The electric continuity properties of zinc-plated steel is different from ordinary steel. When spot welding, increase the current by 10-20%, or increase the resistance welding time. Also increase the number of weld spots by 20-30%.
NOTE: The MIG welding procedures for zinc-plated steel are the same as for ordinary steel plate.
WARNING: To prevent eye injury and burns when welding, wear an approved welding helmet, gloves and safety shoes.
- Before applying putty or body filler to the zinc-plated steel, sand the zinc plating thoroughly to promote adhesion and prevent blistering.
NOTE: Use only epoxy-based putties and fillers on zinc-plated steel. Follow the manufacturer’s specification.
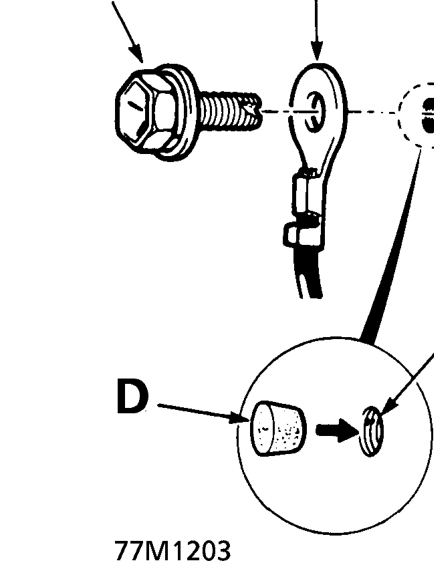
A Special Bolt B Ground Wire C Ground Wire Mounting Hole D Caulking
- When performing paint work, apply masking tape to the ground wire mounting position on the body.
Parts & tools for this job For 1995 Rover 400
- TOOLTrim removal tool kitSearch: trim removal tool kit
- PARTTouch-up paintSearch: Rover touch up paint
- PARTPanel clip assortmentSearch: Rover panel clips assortment
Links open Amazon search results in a new tab. As an Amazon Associate I earn from qualifying purchases.