Power transmissionSecondary shaft: dismounting and assembling
| Secondary shaft: dismounting and assembling |
| t
| If it is necessary to assemble new pinions, consult section Identification initials, assignation of groups, reductions, amounts for filling → Chapter. |
| t
| The secondary shaft must always be adjusted when parts have been replaced that might affect the position of the tapered roller bearings. Consult the Chart for Adjustments → Chapter. |
|
q
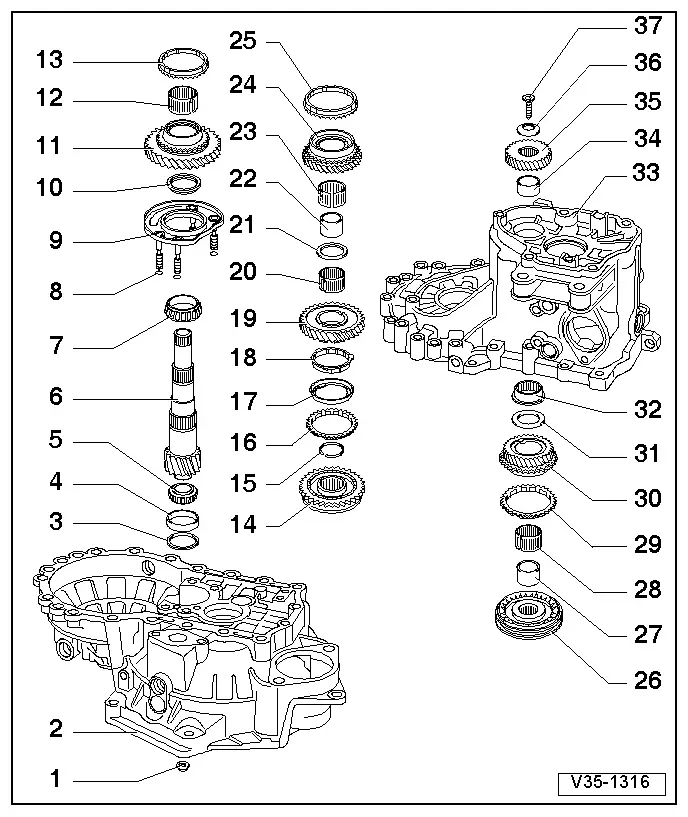
| For attaching the secondary shaft |
|
q
| For the secondary shaft |
| 4 - | Outer track, tapered roller bearing |
| 5 - | Tapered roller bearing |
|
q
| It is coupled with the pinion for the control drive trains; in the event of replacement they should be changed together. |
|
q
| In the event of replacement ï Identification initials, assignation of groups, reductions, amounts for filling → Chapter |
|
q
| Adjustment for the secondary shaft → Chapter |
| 7 - | Tapered roller bearing |
|
q
| For the bolts for attaching the cover for the secondary shaft bearing → Item |
| 9 - | Cover for the secondary shaft bearing |
|
q
| It includes the outer track for the tapered roller bearing → Item. |
|
q
| The cover for the secondary shaft bearing must be replaced together with the outer track for the tapered roller bearing and the tapered roller bearing → Item. |
|
q
| The edge of the washer must be facing towards the tapered roller bearing. |
|
q
| Before assembling the 1st gear pinion assemble the stop washer → Item. |
| 12 - | Needle bearing for 1st gear pinion |
| 13 - | Synchroniser ring for 1st gear |
|
q
| Check that the flanges have no signs of wear. |
| 14 - | Synchroniser unit for 1st and 2nd gears |
|
q
| Dismounting the secondary shaft → Fig.. |
|
q
| Position for assembly → Fig.. |
|
q
| Assembly of the secondary shaft → Fig.. |
|
q
| Use tool -A-81124- for extracting the safety ring. |
| 16 - | Outer synchroniser ring for 2nd gear |
|
q
| Assembly: the trimmings of the synchroniser ring must always be fitted with the pins in the synchroniser unit for 1st and 2nd gear → Item. |
| 17 - | Intermediate synchroniser ring for 2nd gear |
|
q
| Place it on the outer synchroniser ring → Item. |
|
q
| Position for assembly → Fig.. |
|
q
| Replace it if it shows signs of wear or cracks. |
| 18 - | Inner synchroniser ring for 2nd gear |
|
q
| Check that the flanges do not show any signs of wear. |
|
q
| Position for assembly → Fig.. |
|
q
| Position for assembly → Fig.. |
| 20 - | Needle bearing for 2nd gear pinion |
| 22 - | Sleeve for needle bearing |
|
q
| Dismounting, together with the 2nd gear pinion → Fig.. |
| 23 - | Needle bearing for 3rd gear pinion |
| 25 - | Synchroniser ring for 3rd gear |
| 26 - | Synchroniser unit for 3rd and 4th gears |
|
q
| Dismounting the secondary shaft → Fig.. |
|
q
| Dismounting the synchroniser unit → Fig. |
|
q
| Position for assembly → Fig. |
|
q
| Assembly for the secondary shaft → Fig.. |
| 27 - | Casquilho Sleeve for needle bearingrolamento de agulhas |
|
q
| Dismounting together with the synchroniser unit for 3rd and 4th gears → Item, → Fig. |
| 28 - | Needle bearing for 4th gear pinion |
| 29 - | Synchroniser ring for 4th gear |
| 32 - | Needle bearing for the secondary shaft |
| 34 - | Sleeve for needle bearing |
|
q
| Position for assembly: the concave side must remain facing towards the 5th gear pinion. |
| 37 - | Bolt for attaching the 5th gear pinion |
|
q
| The head of the bolt includes a housing for the plate spring → Item |

| Special tools and workshop equipment required |
| t
| Case for extractors for gearboxes -U-40100- |
| t
| Gearbox repair case -U-40200- |
| t
| Gearbox repair case -U-40300- |
| t
| Pliers for opening elastic rings -A-81124- |
| Dismounting the outer track for the tapered roller bearing |
| –
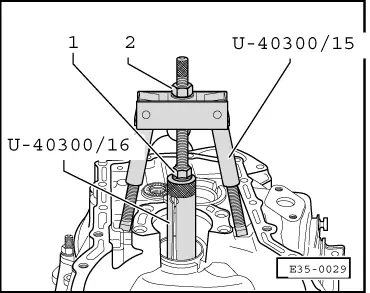
| Dismount the outer track for the tapered roller bearing by carrying out the following steps: |
| –
| Assemble the grips -U-40300/17- on the tool -U-40300/16- using its attachment bolts. |
| –
| Place the set of tools on the lower part of the outer track of the tapered roller bearing. Expand the tool -U-40300/16- by tightening the bolt -1-. |
| –
| Place the extractor tool -U-40300/15- on the clutch casing and tighten the axle of the extractor in the tool -U-40300/16-. |
| –
| Turn the nut -2- until extracting the outer track of the tapered roller bearing. |
|
|
|
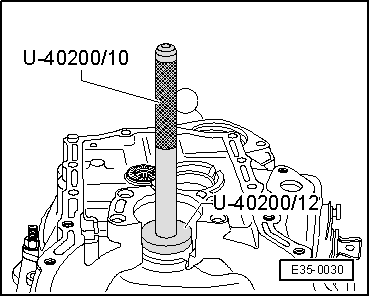
| Assemble the outer track of the tapered roller bearing |
| –
| Assemble the outer track of the tapered roller bearing of the secondary shaft, on the clutch casing, with the tool -U-40200/12- and the tool -U-40200/10-. |
|
|
|
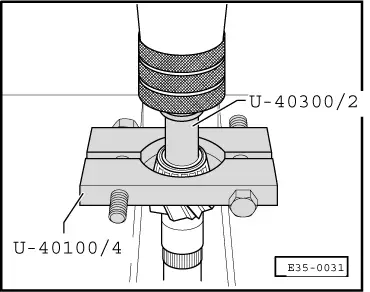
| Dismounting the tapered roller bearing |
| –
| Assemble the tool -U-40100/4- on the secondary shaft anderneath the front pinion. |
| –
| Place the secondary shaft and the tool -U-40300/2- on the press, as is shown on the drawing. |
| –
| Work the press until the tapered roller bearing is extracted. |
|
|
|
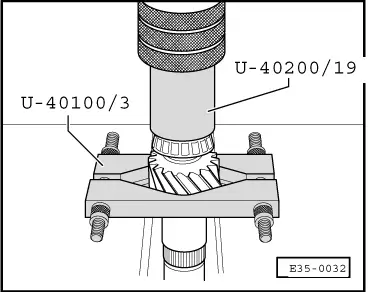
| Assembling the tapered roller bearing |
| –
| Assemble the tool -U-40100/3- on the secondary shaft anderneath the front pinion. |
| –
| Place the tool-U-40200/19- on the press as is shown on the drawing. |
| –
| Work the press until the tapered roller bearing is mounted in its position. |
|
|
|
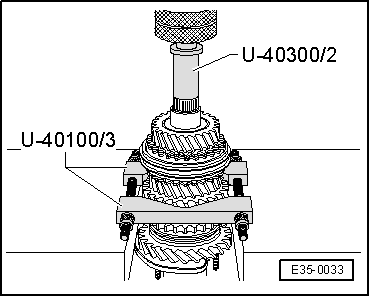
| Dismounting the sleeve for the needle bearing, the 4th gear pinion, the synchroniser unit for 3rd and 4th gears and the 3rd gear pinion of the secondary shaft |
| The 3rd gear pinion will be assembled jointly with the sleeve for the needles bearing, the 3rd and 4th gear synchroniser unit and the 4th gear pinion. |
| –
| Place the tool -U-40100/3- on the secondary shaft ander the 3rd gear pinion. |
| –
| Place the secondary shaft with the tool -U-40100/3- on the press as is shown in the drawing. |
| –
| Work the press and extract at the same time the sleeve for the needle bearing, the 4th gear pinion, the synchroniser unit for 3rd and 4th gears and the 3rd gear pinion. |
|
|
|
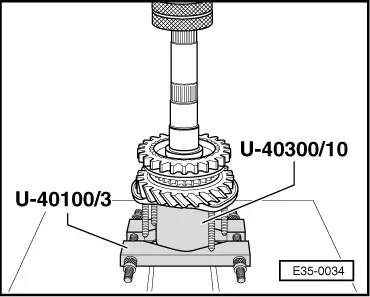
| Dismounting the sleeve for the needle bearing, the 2nd gear pinion, the synchroniser unit for 1st and 2nd gears and the 1st gear pinion of the secondary shaft |
| –
| Remove the safety ring using the tool -A-81124-. |
| –
| Assemble the tools -U-40100/3- and -U-40300/10- on the secondary shaft anderneath the 2nd gear pinion. |
| –
| Put the secondary shaft and the tools -U-40100/3- and -U-40300/10- over the press, as is shown. |
| –
| Work the press and extract at the same time the sleeve for the needle bearing, the 2nd gear pinion, the synchroniser unit for 1st and 2nd gears and the 1st gear pinion of the secondary shaft. |
|
|
|
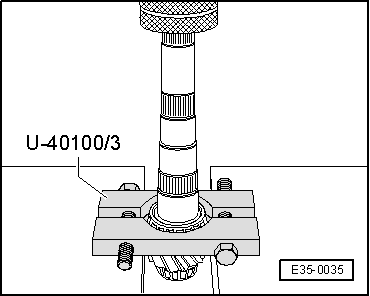
| Dismounting the tapered roller bearing |
| –
| Assemble the tool -U-40100/4- anderneath the tapered roller bearing |
| –
| Place the tool -U-40100/4- over the press, as is shown. |
| –
| Work the press until extracting the tapered roller bearing. |
|
|
|
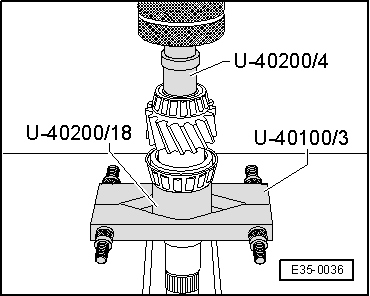
| Assembling the tapered roller bearing |
| –
| Assemble the tools -U-40100/3- and -U-40200/18- with side -A- facing towards the tapered bearing, over the secondary shaft. |
| –
| Place the secondary shaft using tools -U-40100/3- and -U-40200/18- over the press, as shown in the drawing. |
| The side with the smallest external diameter of the tapered roller bearing must be facing towards tool -U-40200/18-. |
| –
| Put the tool -U-40200/4- between the press and the secondary shaft. |
| –
| Work the press until the tapered roller bearing is mounted in its position. |
|
|
|
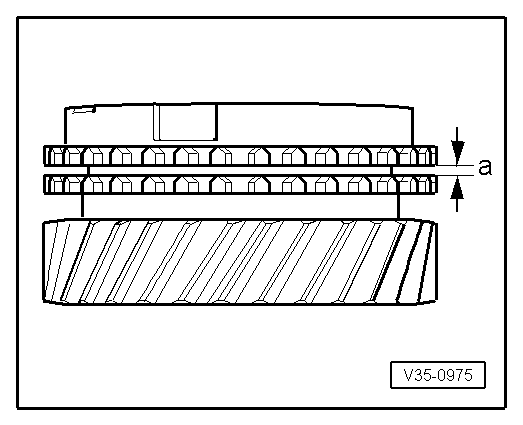
| Control for wear on the synchroniser rings for the 1st, 3rd and 4th gears |
| –
| Before the control for wear, carefully clean the synchroniser rings and their corresponding pinions. |
| –
| Place the synchroniser ring onto the cone of the corresponding pinion. Press down the synchroniser onto the pinion and measure the gap height “a” with a gauge. |
|
|
|
| Synchroniser ring | Measurement “a” in a new synchroniser | Wear limit |
1st gear
3rd gear
4thgear | 1.0 … 1.7 mm | 0.5 mm |
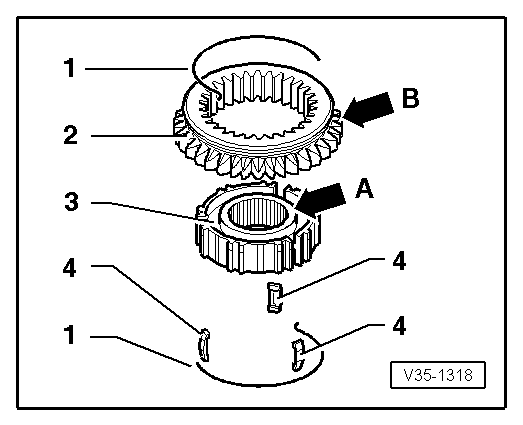
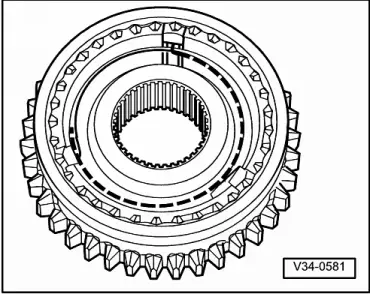
| Dismounting and assembling the synchroniser unit for 1st and 2nd gears |
| –
| In order to dismount the synchroniser unit for 1st and 2nd gears, remove the springs -1- and move the movable sleeve -B- completely upwards. |
| –
| Assemble the synchroniser unit for 1st and 2nd gears by carrying out the following steps: |
| –
| Place the movable sleeve -2- onto the synchroniser hub -3- so that the trimmings for housing the blocking pins -4- for both components coincide. |
| –
| Mount the movable sleeve over its boss in such a way that after they are assembled they will be located so that the widest collar of the synchroniser boss -A- and the inner teeth of the movable sleeve -B- are facing in opposite directions. |
| –
| Assemble the blocking pins -4- and fix them into place with the springs -1- placing them at 120° from each other. |
|
|
|
| Dismounting and assembling the synchroniser unit for 1st and 2nd gears |
| –
| With the synchroniser unit assembled, mount the springs at 120° from each other. The bent ends of the springs must remain inside the blocking pins. |
|
|
|
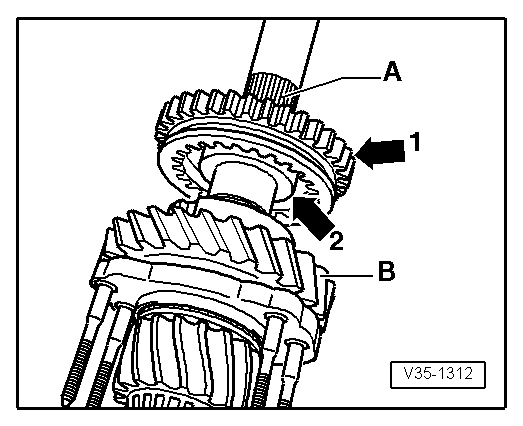
| Position for assembling the synchroniser unit for 1st and 2nd gears |
| –
| The cogs -1- of the movable sleeve must be facing towards the gear teeth -A- for housing the synchroniser unit for 3rd and 4th gears. |
| –
| The collar -2- of the synchroniser hub must be facing towards the pinion -B- for the 1st gear. |
|
|
|
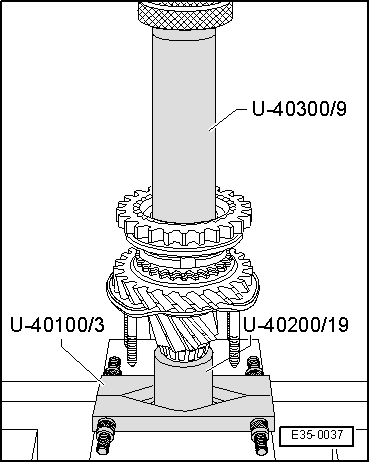
| Assembly of the synchroniser unit for the 1st and 2nd gears in the secondary shaft |
| –
| Place the synchroniser ring for the 1st gear on the 1st gear pinion. |
| –
| Assemble the synchroniser unit for the 1st and 2nd gears in the secondary shaft by carrying out the following steps: |
| –
| Place the tool -U-40100/3- and the tool -U-40200/19- in a press with side A facing upwards. |
| –
| Place the secondary shaft on the tool -U-40200/19-. |
| –
| Place the tool -U-40300/9- between the press and the secondary shaft. |
| –
| Turn the synchroniser ring so that the parts of the block for the synchroniser unit coincide with the housings of the pins for the synchroniser ring. |
| –
| Work the press until the synchroniser unit for the 1stand 2nd gears is mounted in its position. |
| –
| Mount the safety ring using the tool -A-81124- → Item. |
|
|
|
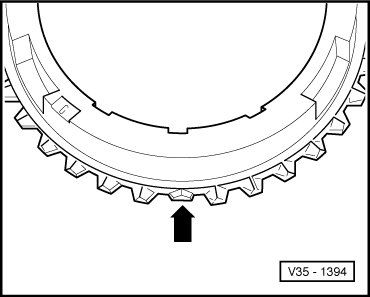
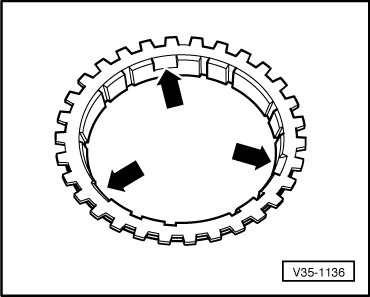
| Identification of the synchroniser rings for 1st and 2nd gears |
| –
| Synchroniser ring for 1st gear: 3 cogs cut down to half size -arrow-. |
| –
| Synchroniser ring for 2nd gear: 2 or 3 cogs cut down to half size -arrow-. |
| –
| The synchroniser ring for the 2nd gear is only supplied as a spare part, with 2 cogs cut down to half size. |
|
|
|
| Identification of the synchroniser rings for 1st and 2nd gears |
| –
| Synchroniser ring for 2nd gear: 3 trimmings -arrows-. |
| –
| Synchroniser ring for 1st gear: without trimmings. |
|
|
|
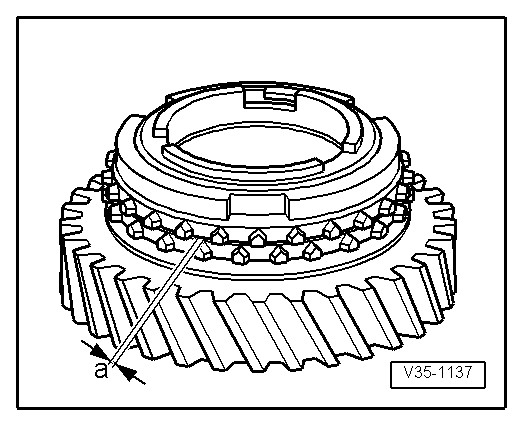
| Control for the wear on the outer synchroniser ring for the 2nd gear |
| –
| Before the control for wear, carefully clean the synchroniser rings and their corresponding pinions. |
| –
| Place the synchroniser ring onto the cone of the corresponding pinion. Press down the synchroniser onto the pinion and measure the gap “a” with a gauge. |
|
|
|
| Synchroniser ring | Measurement “a” in a new synchroniser | Wear limit |
| 2nd gear | 1.2 … 1.8 mm | 0,5 mm |
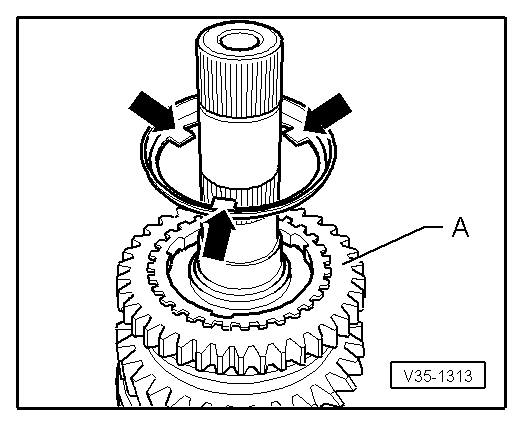
| Position for the assembly of the intermediate synchroniser ring for the 2nd gear |
| –
| The bosses -arrows- must be facing towards the pinion for 1stgear -A-. |
|
|
|
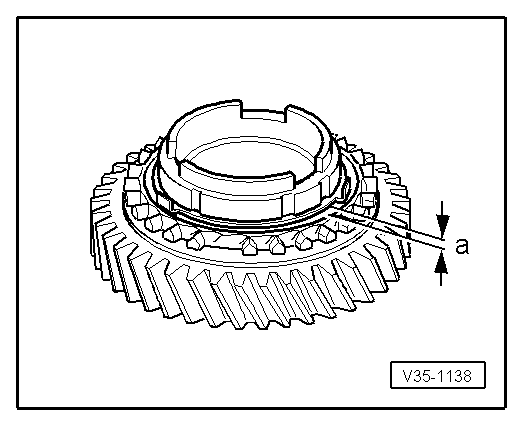
| Control for the wear on the inner synchroniser ring for the 2nd gear |
| –
| Before the control for wear, carefully clean the synchroniser rings and their corresponding pinions. |
| –
| Place the synchroniser ring onto the cone of the corresponding pinion. Press down the synchroniser onto the pinion and measure the gap “a” with a gauge. |
|
|
|
| Synchroniser ring | Measurement “a” in a new synchroniser | Wear limit |
| 2nd gear | 0.75 … 1.25 mm | 0,3 mm |
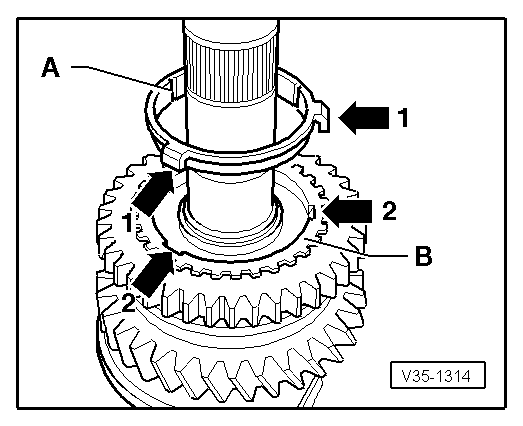
| Position for the assembly of the inner synchroniser ring for 2nd gear |
| –
| The bosses -arrows 1- of the synchroniser ring for the 2nd gear -A- must fit in the trimmings -arrows 2- of the synchroniser ring -B-. |
|
|
|
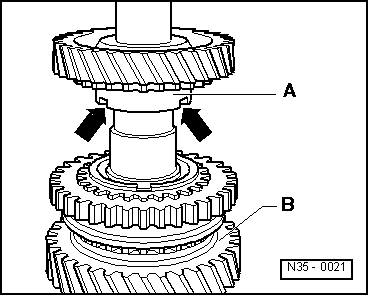
| Position for assembling the 2nd gear pinion |
| –
| The collar -A- of the 2nd gear pinion must be facing towards the 1st gear -B- pinion. |
| –
| The trimmings arrows of the 2nd gear pinion -A- must fit into the bosses of the intermediate synchroniser ring → Fig.. |
|
|
|
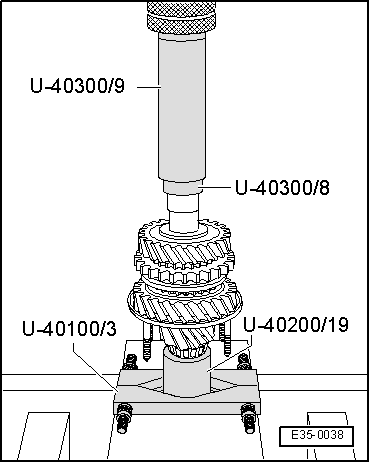
| Assembling the sleeve for the needle bearing |
| –
| Assemble the needle bearing for the 2nd gear pinion and the stop washer in the secondary shaft. |
| –
| Place the tool -U-40100/3- and tool -U-40200/19- in a press with side -A- facing upwards. |
| –
| Place the secondary shaft onto the tool -U-40200/19-. |
| –
| Place the tool -U-40300/8- with side -B- facing towards the sleeve and the tool -U-40300/9-, between the press and the secondary shaft. |
| –
| Work the press until the sleeve for the needle bearing is mounted in its position. |
|
|
|
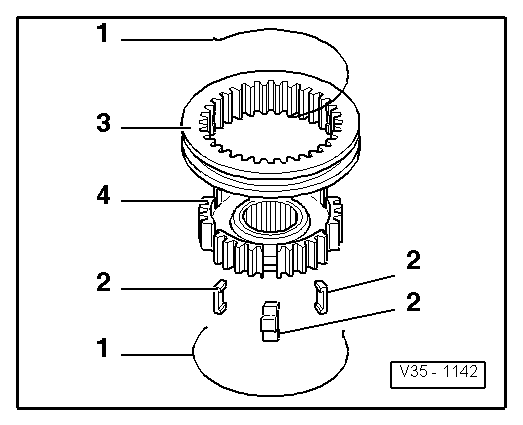
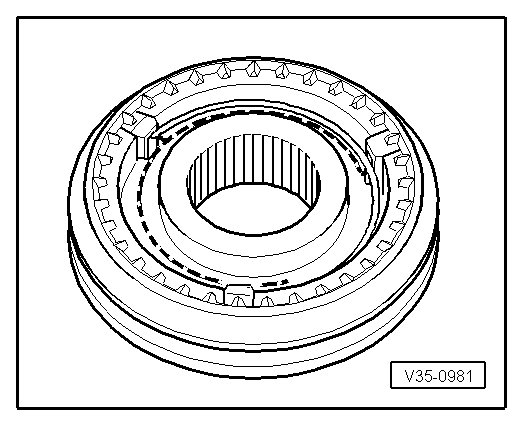
| Dismounting and assembling the synchroniser unit for 3rd and 4th gears |
| –
| In order to dismount the synchroniser unit for 3rd and 4th gears, remove the springs -1and move the movable sleeve -3completely upwards. |
| –
| Assemble the synchroniser unit for 3rd and 4th gears by carrying out the following steps: |
| –
| Place the movable sleeve -3- onto the synchroniser hub -4- so that the trimmings for housing the blocking pins -2- for both components coincide. |
| –
| Assemble the blocking pins -2- and fix them into place with the springs -1- placing them at 120° from each other. |
|
|
|
| Dismounting and assembling the synchroniser unit for the 3rd and 4th gears in the secondary shaft |
| –
| The movable sleeve must be mounted on the synchroniser hub. |
| –
| Place the springs at 120° from each other. The bent ends of the springs must remain inside the blocking pins. |
|
|
|
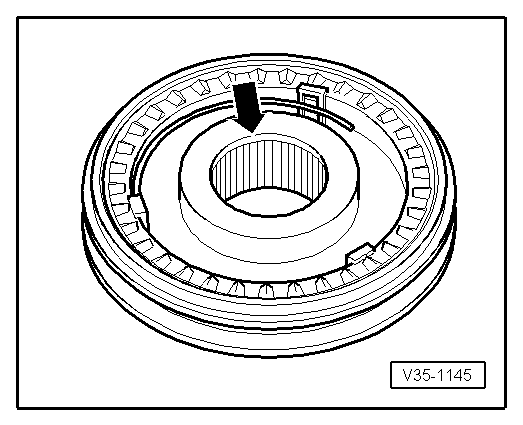
| Position for assembling the synchroniser unit for 3rd and 4th gears |
| –
| The collar with bevel -arrow- of the synchroniser hub must be facing towards the 4th gear pinion. |
|
|
|
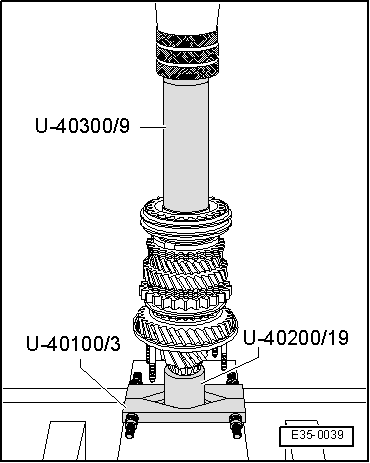
| Assembly of the synchroniser unit for the 3rd and 4th gears in the secondary shaft |
| –
| Assemble the synchroniser unit for the 3rd and 4th gears in the secondary shaft by carrying out the following steps: |
| –
| Assembling o casquilho para rolamento de agulhas. |
| –
| Place the secondary shaft on the tool -U-40200/19-. |
| –
| Situar o utensílio-ferramenta -U-40300/9- entre a prensa e o veio secundário. |
| –
| Turn the synchroniser ring so that the parts of the block for the synchroniser unit coincide with the housings of the pins in the synchroniser ring. |
| –
| Work the press until the synchroniser unit for the 3rd and 4th gears is mounted in its position. |
|
|
|
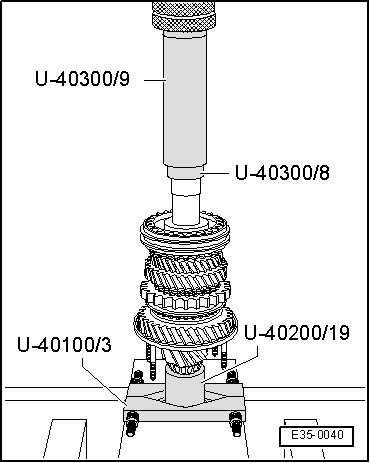
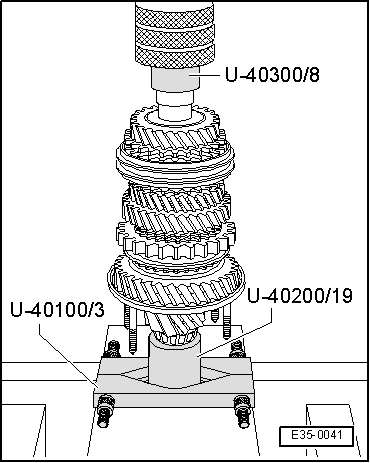
| Assembling the sleeve for the needle bearing |
| –
| Place the tool -U-40100/3- and the tool -U-40200/19- in a press with side A facing upwards. |
| –
| Place the secondary shaft on the tool -U-40200/19-. |
| –
| Place the tool -U-40300/8- with side -B- facing towards the sleeve and tool -U-40300/9-, between the press and the secondary shaft. |
| –
| Work the press until the sleeve for the needle bearing is mounted in its position. |
|
|
|
| Assembling the sleeve for the needle bearing |
| –
| Place the tool -U-40100/3- and the tool -U-40200/19- in a press with side A facing upwards. |
| –
| Place the secondary shaft on the tool -U-40200/19-. |
| –
| Place the tool -U-40300/8- with side A facing towards the sleeve, between the press and the secondary shaft. |
| –
| Work the press until the sleeve for the needle bearing is mounted in its position. |
|
|
|
01 Transmission
The same page in:
Leon Mk2.