Indications to be followed when spot welding.
- Make
- Alfa Romeo
- Model
- 145/146 Factory Service Manual
- Year
- 1994–1999
- Section
- Body - Generalities › Indications to be followed when spot welding.
Indications to be followed when spot welding.
a. Welding of three or more overlapping metal sheets. - When three or more overlapping sheets are to be welded, welding should be repeated a second time.
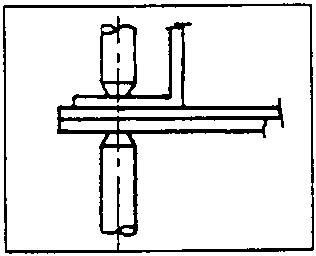
b. Number of spot-welds. - Weld in accordance with the number of spots indicated in this manual.
c. Minimum distance between spot welds and the edge of the sheet metal. - When welding near the edges of the metal sheet the values given in the following table should be used.
| Thickness of sheet metal (t) mm | Minimum distance from the edge of the metal sheet (l) mm |
|---|---|
| 0.6 | 11 |
| 0.8 | 11 |
| 1.0 | 12 |
| 1.2 | 14 |
| 1.6 | 16 |
| 1.8 | 17 |
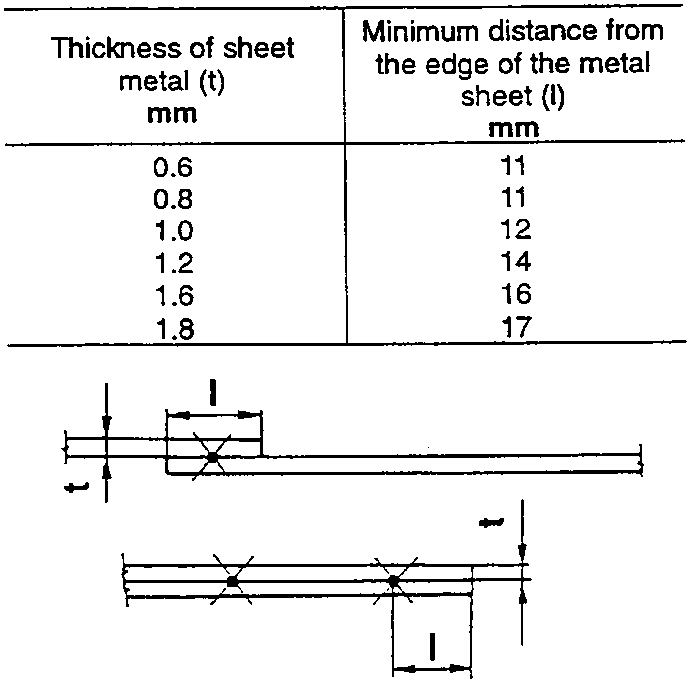
Welding carried out too close to the edge will not be strong enough and sheets may warp.
d. Welding sequence. - Do not weld in one direction only as this results in weak welds due to electricity shunting. If the electrodes overheat and change colour interrupt the operation, leave them to cool and reshape the tips.
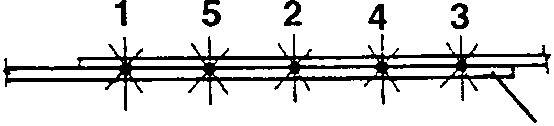
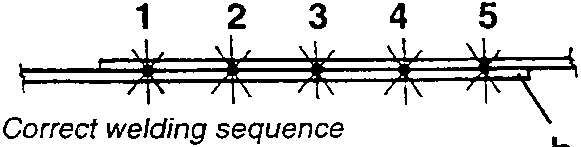
a. Correct welding sequence b. Incorrect welding sequence
e. Welding on angled surfaces. - Do not weld on angled surfaces as a concentration of voltage is created which can cause breakage.
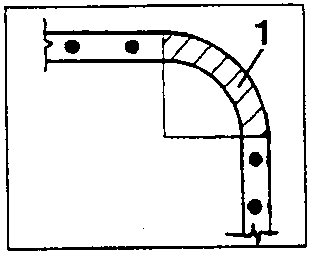
- Angular surfaces exempt from welding.
Examples: - Front pillar upper corner. - Front part of rear wing. - Front and rear window corners.
Inspecting the welding areas.
The spot-welding areas can be inspected either visually or by using a destructive method. This last method should be applied before and after welding. Spot-welds should be equally spaced and positioned at the centre of the flange.
a. Sample test to be carried out before welding. - Prepare the samples using metal sheet of the same thickness as the parts to be welded and secure them so that they do not move during welding. Carry out welding. - Rotate the samples around the spot-weld until they detach and then inspect the break. - The entire spot-weld should remain on one of the two samples and a circular hole should be on the other. If this condition is not met welding conditions are incorrect. Adjust the pressure, electricity and electricity flow time and other welding parameters and repeat the test until better results are obtained.
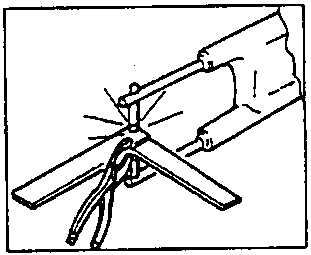
Correct welding parameters
Incorrect welding parameters
Parts & tools for this job For 1994 Alfa Romeo 145/146
- TOOLTrim removal tool kitSearch: trim removal tool kit
- PARTTouch-up paintSearch: Alfa Romeo touch up paint
- PARTPanel clip assortmentSearch: Alfa Romeo panel clips assortment
Links open Amazon search results in a new tab. As an Amazon Associate I earn from qualifying purchases.