Engine - dismantle and reassemble following operation 1004e10 - wash and check dismantled parts - refit cylinder head an
- Make
- Fiat
- Model
- Croma Factory Service Manual
- Year
- 2005–2010
- Section
- Engine and power unit › Engine - dismantle and reassemble following operation 1004e10 - wash and check dismantled parts - refit cylinder head an
ENGINE - DISMANTLE AND REASSEMBLE FOLLOWING OPERATION 1004E10 - WASH AND CHECK DISMANTLED PARTS - REFIT CYLINDER HEAD AND OIL SUMP - DOES NOT INCLUDE REPAIRS TO CYLINDER HEAD AND AUXILIARY UNIT
Removing
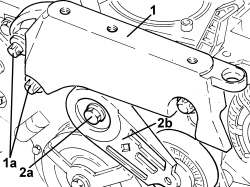
1. Undo the bolts (1a) and remove the rigid power unit support (1b).
2. Undo the bolt (2a) and remove the auxiliary unit drive belt (2b).
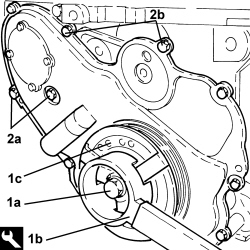
1. Undo the bolt (1a) using the tool (1b) for counter-torque and remove the crankshaft pulley (1c).
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000001000 | Counter-torque | Loosen/tighten crankshaft pulley fixing bolt | 2.2 |
2. Undo the bolts (2a) and remove the timing chain cover (2b).
- Remove the gasket.
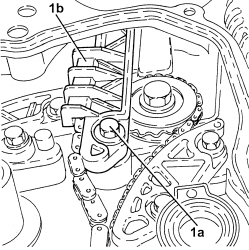
1. Undo the bolt (1a) and remove the timing chain fixed pad (1b).
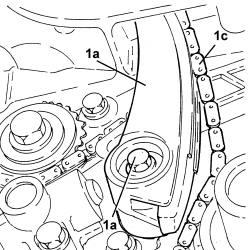
1. Undo the bolt (1a) and remove the moving pad (1b) and the timing chain (1c).
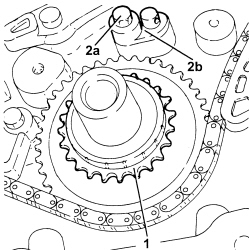
1. Release the timing chain toothed wheel.
2. Undo the bolt (2a) and remove the timing chain (2b) lubrication jet.
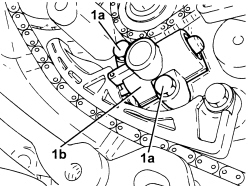
1. Undo the bolts (1a) and remove the counter-balance shaft chain hydraulic belt tensioner (1b).
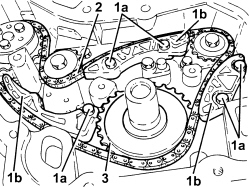
1. Undo the bolts (1a) and remove the three counter-balance shaft chain pads (1b).
2. Remove the counter-balance shaft chain.
3. Release the counter-balance shaft chain toothed wheel.
1. Undo the bolts (1a) and remove the two counter-balance shafts (1b).
The inlet side counter-balance shaft has a green paint mark and the exhaust side one has a white paint mark.
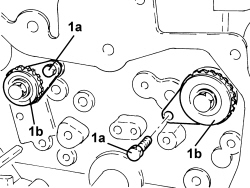
1. Undo the bolts (1a) and remove the water pump gear (1b).
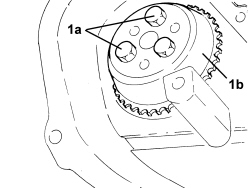
1. Undo the fastenings (1a) and remove the thermostat complete with coolant temperature sensor and rigid supply pipe to the water pump (1b).
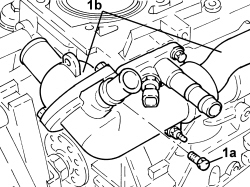
1. Undo the fastenings (1a) and remove the water pump cover (1b).
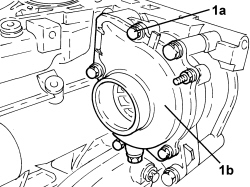
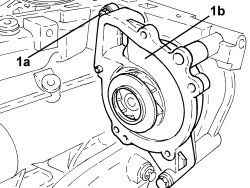
1. Undo the bolts (1a) and remove the pump casing (1b).
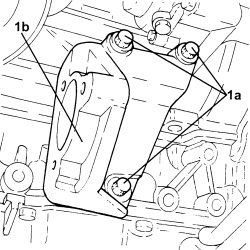
1. Undo the bolts (1a) and remove the intermediate shaft support (1b).
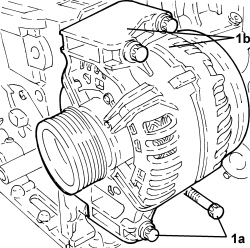
1. Undo bolts (1a) and remove alternator (1b).
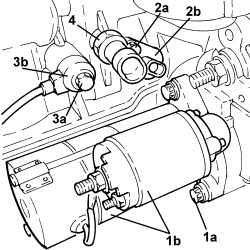
1. Undo the bolts (1a) and remove the starter motor (1b).
2. Undo the bolt (2a) and remove the rpm sensor (2b).
3. Undo the bolt (3a) and remove the detonation sensor (3b).
4. Undo and remove the engine oil pressure warning light switch.
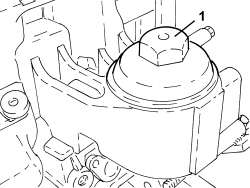
1. Undo and remove the engine oil filter cartridge cap.
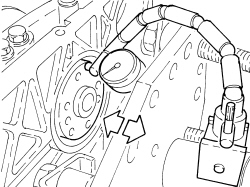
- Check that the crankshaft endfloat corresponds to the recommended figures using a magnetic base and dial gauge.
| Measurement | Value | Validity |
|---|---|---|
| Crankshaft endfloat (mm) | 0.092 ÷ 0.240 | 2.2 16V |
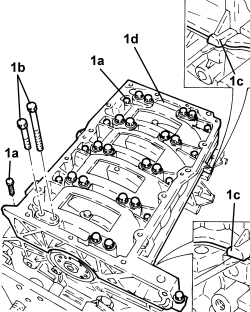
1. Undo the outer bolts (1a), undo the double row of inner bolts (1b) and remove the sealant at the two preset points (1c) and remove the panel under the crankcase (1d).
Pay attention to the fitting position of the panel under the crankcase.
- Remove the flywheel side crankshaft seal.
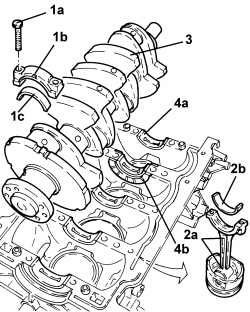
1. Undo the bolts (1a) and remove the connecting rod caps (1b) and half-bearings (1c).
2. Remove the piston-connecting rod assemblies (2a) complete with half-bearings (2b).
Mark the connecting rod and cap and pay attention to the cylinder sequence. The breaking surfaces of the connecting rod and the cap match individually and therefore cannot be swapped or damaged. Do not exert pressure to the breaking surfaces.
3. Remove the crankshaft.
4. Remove the crankshaft half bearings (4a) and the thrust washers (4b).
- Remove the locating bushes for the cylinder block/crankcase.
1. Undo the engine oil duct plugs (1a) and the water duct plugs (1b).
Refitting
- Wash all the dismantled components thoroughly.
- Clean the matching surfaces between the oil sump and the panel under the crankcase and between the panel under the crankcase and the crankcase.
- Refit the threaded plugs for the water and engine oil ducts.
- Lubricate all the mechanical components with engine oil.
- Visually check that the cylinder head support surface does not have cracks or superficial grooves.
- Check that the internal diameter of the cylinder liners is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner bore | 85.992 - 86.008 mm | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner oversize | 86.117 - 86.133 mm | 2.2 16V |
- Check that the diameter of the main journals corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter (mm) | 55.994 ÷ 56.008 | 2.2 16V |
- Check that the diameter of the crankpins corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter (mm) | 49.000 ÷ 49.014 | 2.2 16V |
- Check the matching between the gudgeon pin and the housing in the piston; it should be possible to insert the pin simply by pressing and it should not slip out. Check that the outer diameter of the gudgeon pins is within the recommended limits; if not, replace the worn gudgeon pins.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin outer diameter (mm) | 19.995 ÷ 20.000 | 2.2 16V |
- Fit the piston rings in the cylinder bore and check that the opening between the ends is within the recommended values; if this is not the case, replace the circlips.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring gap (mm) | 0.20 ÷ 0.40 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring gap (mm) | 0.35 ÷ 0.55 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Oil scraper ring endfloat (mm) | 0.20 ÷ 0.35 | 1.8 |
- The size of the seals is given below.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring thickness (mm) | 1.17 ÷ 1.19 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring thickness (mm) | 1.47 ÷ 1.49 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring size (mm) | 2.348 ÷ 2.477 | 2.2 16V |
- Check that the outer diameter of the pistons corresponds to the recommended figures; if not, replace the piston complete with piston rings and gudgeon pin.
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter (mm) | 85.967 ÷ 85.982 | 2.2 16V |
- The clearance between the pistons and the liner/bore is given below.
| Measurement | Value | Validity |
|---|---|---|
| Clearance between piston - cylinder liner/bore (mm) | 0.025 ÷ 0.026 | 2.2 16V |
- Check that the endfloat between the seals and the housings in the piston is within the recommended values; if this is not the case, replace the seals with oversize ones.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring endfloat (mm) | 0.06 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring endfloat (mm) | 0.05 | 2.2 16V |
| Measurement | Value | Validity |
|---|---|---|
| Oil scraper ring endfloat (mm) | 0.063 ÷ 0.172 | 2.2 16V |
- Check the main half bearings, noting that the half-bearings should not be adapted. Replace them if scoring or signs of binding are noted.
- Fit the main bearing halves in their seats on the upper crankcase, aligning the lubrication holes and ensuring scrupulous cleanliness. The centre crankshaft bearing has thrust half-washers incorporated becuase it acts as a thrust carrier.
- If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
1. Place the crankshaft in its housing.
2. Fit the calibrated wire for measuring the bearing clearance.
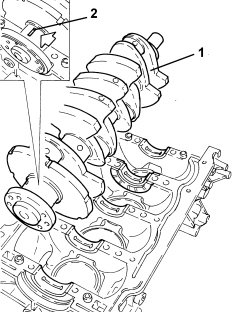
- Fit the main journal half-bearings in the lower cylinder block/crankcase.
1. Fit the lower crankcase on the upper one.
2. Tighten bolts (2a) and bolts (2b) securing the lower crankcase.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Lower engine crankcase | Bolt | M8 X 1.25 | (outer side) 2.3 | 2.2 |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Lower engine crankcase | Bolt | M10 x 1.5 | (inner side) 2.0 +70° +15° | 2.2 |
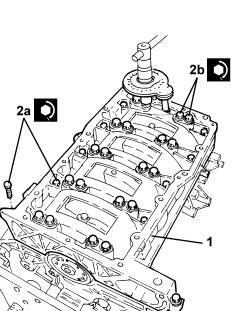
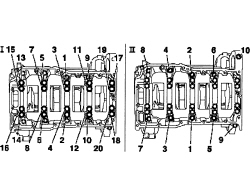
- Bolt tightening sequence (I = M10; II = M8)
1. Remove the lower crankcase and check the crankpin clearance. Use an appropriate gauge to measure the width of the plastigage.
Check one main journal at a time, without rotating the crankshaft.
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main bearings - crankshaft bearings (mm) | 0.007 ÷ 0.014 | 2.2 16V |
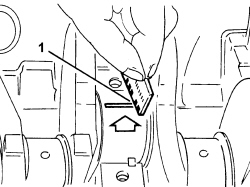
- After having checked all the main journals, apply a bead of sealant about 2 - 5 mm thick in the splining in the crankcase and then proceed with the definitive fitting of the lower crankcase tightening the bolts to torque following the order given previously.
- Fit the flywheel side crankshaft seal.
- Rotate the engine through 180° on the overhaul stand.
- Fit the connecting rod-piston assemblies complete with half bearings in the cylinder liners/bores.
- Rotate the engine through 180° on the overhaul stand.
1. Apply the calibrated wire for measuring the crankpin clearance.
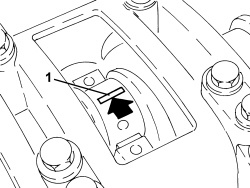
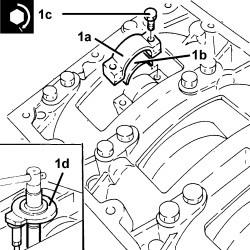
1. Fit the connecting rod caps (1a) complete with half-bearings (1b) and secure by tightening the new bolts (1c) to the specified torque using the torque wrench (1d).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt (to be replaced) | M9 x 1 | (connecting rod side) 2.5 + 50° + 50° + 15° | 2.2 |
1. Remove the connecting rod caps and check the crankpin clearance. Use an appropriate gauge to measure the width of the plastigage.
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main ljournals - crankshaft bearings (mm) | 0.041 ÷ 0.043 | 2.2 16V |
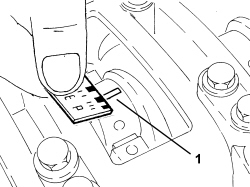
- If the value measured is not within the recommended figures, replace the connecting rod bearings.
- Refit the connecting rod caps complete with half-bearings and secure them by tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt (to be replaced) | M9 x 1 | (connecting rod side) 2.5 + 50° + 50° + 15° | 2.2 |
- Fit a new engine oil filter cartridge.
- Fit the detonation sensor.
- Fit the engine rpm sensor.
- Fit the engine oil pressure warning light switch.
- Place the starter motor in position and secure it.
- Place the alternator in its housing and secure it.
- Position the pump casing in its housing with the pulley and secure it.
- Fit two new seals on the water pump rigid supply pipe.
- Place the thermostat in its housing complete with water pump supply pipe and secure it.
- Place the two counter-balance shafts in their housing and secure them.
1. Fit the toothed wheel (1a), fit the chain (1b) aligning the copper mesh (a) with the arrow on the toothed wheel (1c), the silver mesh (1b) with the letters C-R on the toothed wheel (1a) and lastly the silver mesh (c) with the arrow on the toothed wheel (1d).
2. Place the fixed chain tensioner pads (2a) and the moving pad (2b) in their housings.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Water pump/balancing shafts drive chain pad(s) | Bolt | M6 x 1 | (engine crankcase side) 1.0 | 2.2 |
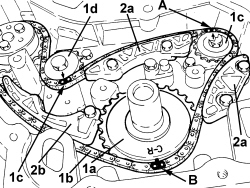
- Preload the hydraulic tensioner for the counter-balance shaft chain and fit it at the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Water pump/balancing shafts drive chain hydraulic tensioner | Bolt | M6 x 1 | (engine crankcase side) 1.0 | 2.2 |
- Fit the chain lubrication jet.
- Clean any residues of gasket from the the cylinder head - engine block matching surfaces.
- Place the cylinder head gasket in position.
The gasket should be positioned with the word "TOP" facing upwards.
- Place the cylinder head in position.
Two mechanics are needed for this operation.
- Check that the centering bushes are correctly positioned.
Take care to raise the timing chain and the exhaust side camshaft drive pulley.
1. Tighten the new cylinder head fixing bolts to the recommended torque using the angular tightening tool.
Follow the order shown in the figure for each tightening sequence.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cylinder head | Bolt (to be replaced) | M11 x 1.5 | (engine crankcase side) 3.0 + 90° +60° +15° | 2.2 |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
2. Tighten the new bolts securing the cylinder head to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cylinder head | Timing side bolts (to replace) | M8 X 1.25 | (engine crankcase side) 3.5 | 2.2 |
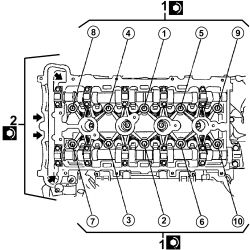
- Tighten the upper bolt fixing the belt tensioner pad to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing fixed chain tensioner pad | Upper bolt | M6 x 1 | (cylinder head side) 0.8 | 2.2 |
- Replace the access plug to the upper belt tensioner bolt in its seat and tighten to the specified torque.
Replace the seal.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cap for timing fixed chain tensioner pad upper bolt | M22 x 1.5 | 6.5 | 2.2 |
- Remove the band used for fastening the timing chain to the exhaust side camshaft toothed drive pulley.
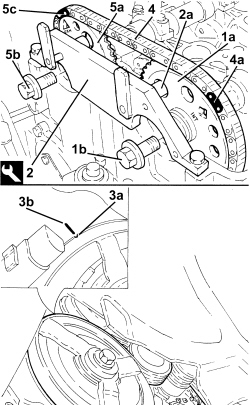
1. Place the intake side camshaft toothed drive pulley (1a) in its housing and secure it with a new bolt (1b) without tightening the bolt.
2. Fit the camshaft timing tools.
Turn the intake side camshaft by means of the hexagon until timing tool pin (2a) fits into the hole on the pulley.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000000900 | Template | Camshaft timing adjustment | 2.2 |
3. If necessary, rotate the crankshaft until cylinder no. 4 is at T.D.C. during the explosion stroke; in this condition the reference (3a) on the inner part of the crankshaft pulley should be aligned with the reference (3b) on the timing chain cover.
Turn the crankshaft slowly and steadily (in the direction of engine rotation).
Ensure the timing chain is not stuck.
4. Fit the timing chain on the inlet side camshaft drive pulley.
The light blue mesh (4a) should be in line with the "INT" mark stamped on the inlet side camshaft drive pulley.
5. Place the exhaust side camshaft toothed drive pulley (5a) in its housing and secure it without tightening the new bolt (5b).
Turn the exhaust side camshaft by means of the hexagon until the pink link (5c) is aligned with the "EXH" mark stamped on the exhaust side toothed timing drive pulley.
- Move back the camshaft timing tool pin from the intake side camshaft toothed timing drive pulley.
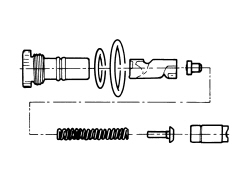
- The following drawing shows the fixed timing chain hydraulic tensioner disassembled.
Replace the seals.
- Before refitting, the timing chain hydraulic tensioner must be preloaded as described below.
1. Position the piston in a vice with protective jaws, holding it by the square end.
2. Insert the piston into the tensioner case by pressing and turning as shown in the figure until the pin (2a) fits into the groove (2b).
3. Press and simultaneously turn the piston until the pin (3a) fits into the groove (3b).
- Insert the assembled piston into the tensioner body.
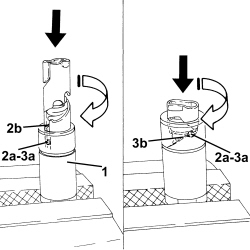
- Refit the timing chain hydraulic tensioner into its seat and tighten to the specified torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing fixed hydraulic tensioner | M27 x 2 | 7.5 | 2.2 |
1. Hydraulic tensioner in operating position.
Move the timing chain hydraulic tensioner to operating position by exercising overall pressure by hand on the chain in the area shown in the figure. This puts the chain under tension, which in turn acts on the mobile pad to release the mobile tensioner piston.
When the tensioner piston is operated, the operating spring can be heard to click.
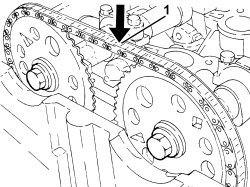
If the chain remains slack, the tensioner is not in the operating position.
- Rotate the crankshaft through 720°, then place cylinder no. 4 at T.D.C. during the explosion stroke; in this condition the reference on the inner part of the crankshaft pulley should be aligned with the reference on the timing chain cover.
When the crankshaft is turned, the tensioner piston should follow the chain through its rotation.
- Check the timing by ensuring that the tool pins are aligned with the holes on the camshaft drive pulleys.
If they do not align, refit the timing chain without treating the coloured links on the chain as TDC reference points.
- Remove the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000000900 | Template | Camshaft timing adjustment | 2.2 |
Place the upper timing chain pad in its housing and fasten it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing upper chain tensioner pad | Bolt (with thread-locking agent) | M6 x 1 | (cylinder head side) 1.0 | 2.2 |
1. Tighten the new camshaft toothed pulley bolts to the specified torque, first tightening the exhaust side pulley bolt.
Turn the hexagonal bolts on the camshafts to provide countertorque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Camshaft toothed drive pullies | Bolt (to be replaced) | M12 x 1.75 | (camshaft side) 8.5 + 30° + 15° | 2.2 |
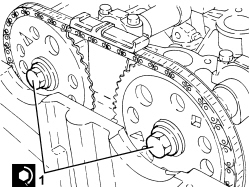
- Place a new gasket back in position.
1. Place the exhaust manifold (1a) in its housing and secure it by tightening the new nuts (1b) to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Exhaust manifold with catalytic converter | Nut (to replace) | (cylinder head side) 2.0 | 1.8 2.2 |
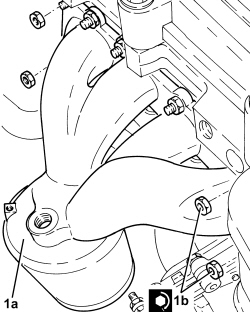
1. Place the heat shield (1a) in its housing and secure it using the bolts (1b).
2. Position the front Lambda sensor in its housing and tighten it to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Front Lambda sensor to catalytic converter | - (with special black grease) | M18 x 1.5 | (exhaust manifold with catalytic converter side) 4.0 | 2.2 |
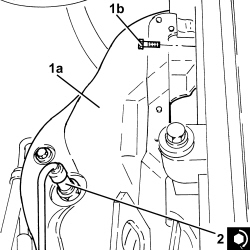
- Place the ignition coil module in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Ignition coil module | Bolt | M6 x 1 | (tappet cover side) 0.9 | 2.2 |
- Connect the electrical connection to the ignition coil module.
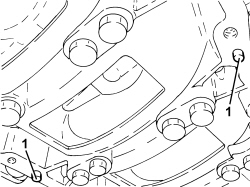
Removing
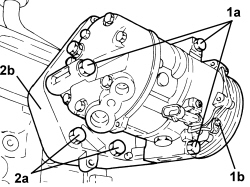
1. Undo the bolts (1a) and remove the air conditioning compressor (1b) from the mounting.
2. Undo the bolts (2a) and remove the air conditioner compressor mounting (2b).
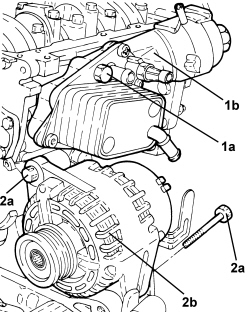
1. Undo the bolts (1a) and remove the engine oil filter and heat exchanger mounting (1b).
2. Undo the bolts (2a) and remove the alternator (2b).
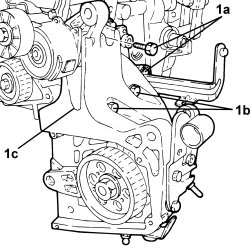
1. Undo the bolts (1a) and (1b), then remove the pressure pump support assembly (1c).
- Remove the locating pins.
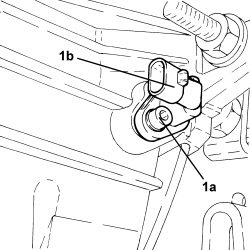
1. Undo the bolt (1a) and remove the rpm sensor (1b).
- Undo the bolts and remove the flywheel side oil seal cover.
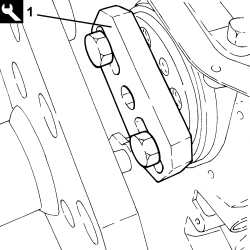
1. Fit the tool for rotating the crankshaft.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
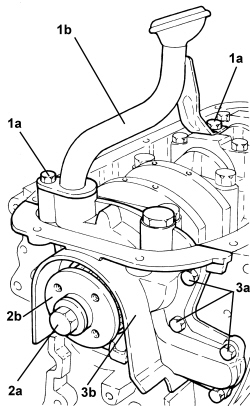
1. Undo the bolts (1a) and remove the engine oil intake (1b).
2. Undo the bolt (2a) and remove the timing toothed drive pulley (2b).
3. Undo the bolts (3a) and remove the crankshaft oil seal front cover (3b).
1. Undo the bolts (1a) and remove the fixed timing tensioners support (1b).
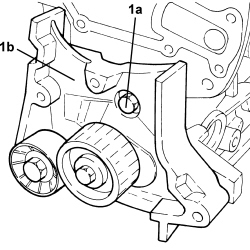
Rotate the crankshaft using the tool fitted previously until the cylinder concerned is at B.D.C.
1. Undo the bolts (1a) and remove the connecting rod cap (1b).
2. Remove the lower connecting rod half-bearing.
3. Remove the connecting rod-piston assembly.
4. Remove the upper connecting rod half-bearing.
Carry out the same operations to remove the pistons and connecting rods for the remaining cylinders.
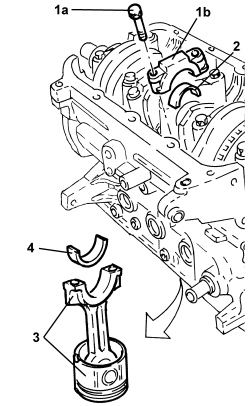
Remove the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
- Check that the crankshaft endfloat corresponds to the recommended figures using a magnetic base and dial gauge.
| Measurement | Value | Validity |
|---|---|---|
| Crankshaft endfloat (mm) | 0.049 ÷ 0.211 | 1.9 JTD 16V |
If the value for the crankshaft endfloat does not correspond with the recommended figures, when refitting, regrind the crankcase seat and use suitable oversize thrust washers.
1. Undo the bolts (1a) and remove the connecting rod caps (1b).
2. Remove the lower main journal half-bearings.
3. Remove the crankshaft.
4. Remove the upper main journal half-bearings.
5. Remove the thrust washers.
6. Undo the bolts (6a) and remove the jets (6b) from the crankcase.
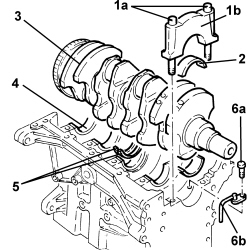
- Remove the cylinder block/crankcase from the support tools, then place on a workbench.
1084B18 POMPA OLIO MOTORE, staccata - Verifica al banco
Drill and remove the water/oil sealing plugs from the crankcase to allow for washing the ducts.
Refitting
Wash the dismantled components.
Fit the water/oil sealing plugs in the crankcase using suitable fitting tools.
Lubricate all the mechanical components with engine oil.
Check that the cylinder head support surface does not have cracks or superficial grooves.
Check that the planarity of the cylinder head support surface corresponds to the recommended figure; if this is not the case, regrind the cylinder head support surface.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder head support surface flatness (mm) | < 0.1 | 1.9 JTD 16V |
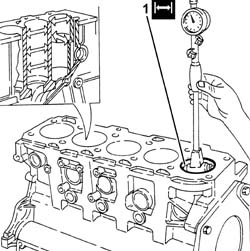
1. Measure the cylinder bore diameter using the diagram illustrated.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade A (mm) | 82.000 ÷ 82.010 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade B (mm) | 82.010 ÷ 82.020 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade C (mm) | 82.020 ÷ 82.030 | 1.9 JTD 16V |
Check that the taper of the cylinder liners is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner taper (mm) | < 0.005 | 1.9 JTD 16V |
Check that the ovality of the cylinder liners is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner ovality (mm) | < 0.05 | 1.9 JTD 16V |
If the cylinder bore measurements are not within the recommended limits, ream the cylinder bores following the recommended oversizes.
In the case of reaming, all the bores must have the same oversize.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner bore diameter oversize (mm) | 0.1 | 1.9 JTD 16V |
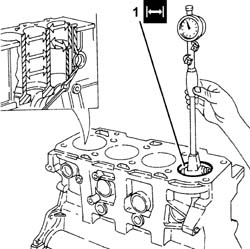
1. Temporarily fit the bearing caps.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
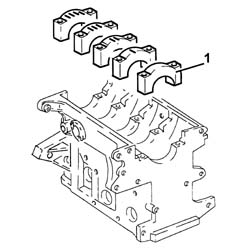
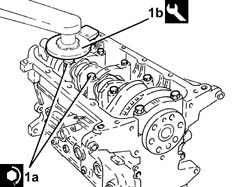
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 1.9 ÷ 2.1 + 100° | 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
2. Check that the diameter of the main journal seats is within specified limits.
| Measurement | Value | Validity |
|---|---|---|
| Main journal seat diameter (mm) | 63.705 ÷ 63.718 | 1.9 JTD 16V |
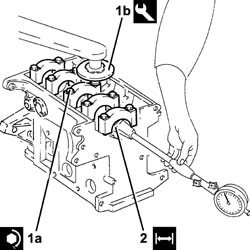
Check that there are no deposits or blockages in the crankshaft lubrication ducts.
Check that the diameter of the main journals is within specified limits.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category A (mm) | 59.994 ÷ 60.000 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category B (mm) | 59.988 ÷ 59.994 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category C (mm) | 59.982 ÷ 59.988 | 1.9 JTD 16V |
If the diameter of the main journals is not correct, they should be reground to the recommended undersize.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter undersize (mm) | 0.127 | 1.9 JTD 16V |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept. The half-bearings used for undersizes of more than 0.127 mm should not be ordered from the Parts Dept. (even if the number is still quoted).
Check that the diameter of the crankpins corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category A (mm) | 50.799 ÷ 50.805 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category B (mm) | 50.793 ÷ 50.799 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category C (mm) | 50.787 ÷ 50.793 | 1.9 JTD 16V |
If the diameter of the crankpins is not correct, they should be reground to the recommended undersize.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter undersize (mm) | 0.127 | 1.9 JTD 16V |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept. The half-bearings used for undersizes of more than 0.127 mm should not be ordered from the Parts Dept. (even if the number is still quoted).
Check the main bearings, noting that the half-bearings should not be adapted. Replace them if scoring or signs of binding are noted.
Fit the half-bearings making sure they are scrupulously clean.
If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
Fit the crankshaft in the crankcase.
1. Fit the calibrated wire (plastigage) for measuring the bearing clearance.
Check one journal at a time, without rotating the crankshaft.
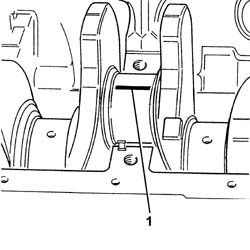
1. Fit the main bearing caps complete with half-bearings.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
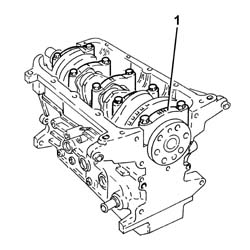
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 1.9 ÷ 2.1 + 100° | 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
1. Remove the bearing caps fitted previously and, using a suitable graduated measuring instrument (1a), measure the clearance shown by the calibrated wire (1b).
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main journals - crankshaft bearings (mm) | 0.011 ÷ 0.071 | 1.9 JTD 16V |
If the figure measured is outside of the tolerance, replace the half-bearings with ones of the correct size and category.
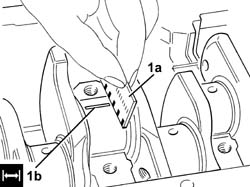
Measure the clearance for all the bearings taking care to take the measurements one at a time without moving the crankshaft at any time.
Check that the small end bush internal diameter is within the recommended limits; if not, replace the worn small end bush.
1028H58 BOCCOLA PIEDE di BIELLA (una) - Sost.
| Measurement | Value | Validity |
|---|---|---|
| Small end bush inner diameter (mm) | 26.006 ÷ 26.014 | 1.9 JTD 16V |
Check that the inner diameter of the gudgeon pin housing in the pistons corresponds to the recommended figures; if not, replace the piston complete with piston rings, gudgeon pin and bushes.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin housing diameter in piston (mm) | 25.999 ÷ 26.004 | 1.9 JTD 16V |
Check that the outer diameter of the piston pins is within the recommended limits; if not, replace the worn piston pins.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin outer diameter (mm) | 25.982 ÷ 25.987 | 1.9 JTD 16V |
Fit the piston rings in the cylinder liner and check that the opening between the ends is within the recommended values; if this is not the case, replace the circlips.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring gap (mm) | 0.20 ÷ 0.35 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring gap (mm) | 0.60 ÷ 0.80 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring gap (mm) | 0.25 ÷ 0.50 | 1.9 JTD 16V |
Check that the outer diameter of the pistons corresponds to the recommended figures; if not, replace the piston complete with piston rings and gudgeon pin.
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter -grade A (mm) | 81.920 ÷ 81.930 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - grade B (mm) | 81.930 ÷ 81.940 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - grade C (mm) | 81.940 ÷ 81.950 | 1.9 JTD 16V |
Measure perpendicular to the gudgeon pin axis, 9 mm from the lower edge of the skirt.
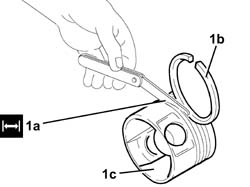
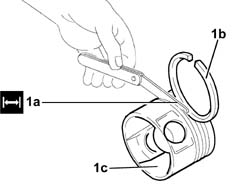
1. Check that the backlash (1a) between the first-second ring (1b) and the seats in the piston (1c) corresponds to the recommeded figures.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring endfloat (mm) | 0.105 ÷ 0.150 | 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring endfloat (mm) | 0.050 ÷ 0.090 | 1.9 JTD 16V |
Check that the backlash between the oil scraper ring and the housing in the piston corresponds to the recommeded figures.
| Measurement | Value | Validity |
|---|---|---|
| Oil scraper ring endfloat (mm) | 0.030 ÷ 0.070 | 1.9 JTD 16V |
1. Fit the caps (1b) on the connecting rods (1a) and secure them tightening the bolts (1c) to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
Use the tool for the angular tightening of the connecting rod cap bolts.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
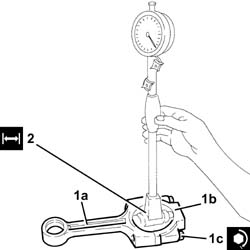
2. - Check that the diameter of the big end corresponds to the recommended figures; if not, replace the connecting rods.
| Measurement | Value | Validity |
|---|---|---|
| Big end inner diameter (mm) | 53.897 ÷ 53.909 | 1.9 JTD 16V |
1084B18 POMPA OLIO MOTORE, staccata - Verifica al banco
Check that there are no signs of seizing on the flywheel ring gear teeth; if this is not the case, replace it.
Place the engine block on the overhaul stand using the mounting bracket.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1871000000 | Overhaul stand | Engine support for overhauling |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1871000000 | Bracket | Positioning engine on overhaul stand |
Place the jets in their housings in the crankcase and secure them using the bolts.
Place the thrust washers in their seats on the third main bearing.
The main journal half-bearings fitted on the crankshaft have been selected for their optimum fitting clearance.
The crankshaft supplied by the Parts Dept. comes without half-bearings and the main journals and crankpins are the "normal" size; the half-bearings to be fitted must therefore be selected identifying the class of each main journal and crankpin for the new crankshaft.
The following must be determined for the selection of main journal half-bearings: the numerical code stamped on the flywheel; the paint mark, if present, next to the main journals.
Below is an example of the identification of main journal grades.
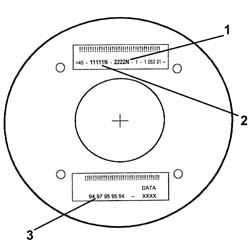
1 - Crankpin identification numerical code: the left number refers to the first timing side bearing; the final "N" is an insignificant code for 4 cylinder engines.
2 - Main journal identification numerical code: the first number refers to the first timing side bearing; the final "N" is an insignificant code for 4 cylinder engines.
3 - Series of numbers (if present), in groups of two digits, which indicate the dimensions (thousandth part) of the main journals: the first two numbers on the left refer to the first timing side bearing
Only use the codes that relate to the key, all other codes on the flywheel should not be used.
For the identification of the main journal grade, refer to the numerical code for reference 2 in the key.
In the case of the example, the numbers 11111N indicate that all five bearings are Grade A (red) as indicated below.
A further method for identifying the grade of the bearings is to read reference 3 (if present) in the diagram.
In the case of the example, the number 94 (first on the left) corresponds to the dimensions 52.994 for the first timing side bearing which identifies Grade A (red); the same method should be applied for other groups of two digits for the same reference 3 (97 -95 -95 -94).
MAIN JOURNAL IDENTIFICATION
Main journal grade A (normal), diameter 59.994.60.000 mm, RED paint mark, numerical code 1 (94 00)*
Main journal grade B (normal), diameter 59.988.59.994 mm, BLUE paint mark, numerical code 2 (88 94)*
Main journal grade C (normal), diameter 59.982.59.998 mm, YELLOW paint mark, numerical code 3 (82 88)*
Main journal grade D (0.127 mm undersize), diameter 59.867.59.873 mm, BROWN paint mark, numerical code 6 (67 73)*
Main journal grade E (0.127 mm undersize), diameter 59.861.59.867 mm, GREEN paint mark, numerical code 7 (61 67)*
Main journal grade F (0.127 mm undersize), diameter 59.855.59.861 mm, BLACK paint mark, numerical code 8 (55 61)*
(*): Last two numbers (thousandth part) of the main journal dimensions.
- In the case of the usage of a crankshaft where the maximum undersize for the bearings is 0.127 mm through grindings, the grade should be selected through the measurement of the diameter of the bearing using the above as a reference.
Having defined the grade and the colour of each new or reground crankshaft bearings, it is necessary to select the thickness of the bearings that should be the same colour as the corresponding bearing; the pair of half-bearings required can be ordered from the Parts Dept. by quoting the order no.
The above is designed to guarantee the optimum operational clearances for all the bearings.
Lastly, we wish to point out that, generally, the clearance between the main journal and the half-bearing, obtained through the selection method indicated above, should be within the following values: Minimum: 0.011 mm - Maximum: 0.071 mm; this value can be measured, as a final check, using the calibrated wire (plastic gauge).
Place the upper main bearing half-bearings in their seats in the engine block.
Place the crankshaft in its housing in the crankcase.
- Place the bearing caps complete with lower half-bearings in position.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
- Tighten the connecting rod cap bolts to the recommended torque using the angular tightening tool.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 1.9 ÷ 2.1 + 100° | 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
- Fit the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
Rotate the crankshaft using the tool fitted previously until the cylinder concerned is at B.D.C.
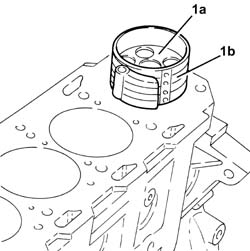
1. Place the piston and connecting rod assembly (1a) in its housing complete with half-bearing using a suitable tool (1b).
For the selection of the connecting rod half-bearings, follow the procedure described previously for the main journal half-bearings.
The piston-connecting rod assemblies should be fitted in the cylinder block/crankcase so that the drain on the piston skirt is aligned with the oil jet on the engine block.
Carry out the same operations to fit the pistons and connecting rods for the remaining cylinders.
1. Test the crankpin clearance by applying plastigage to measure crankpin installation clearance.
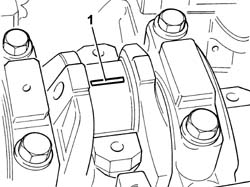
Place the crank pin caps complete with half-bearings in their seats.
Fit the connecting rods so that the number stamped on each rod faces toward the same side as the number stamped on the big end (inlet side).
- Tighten the bolts to the recommended torque, using the angular tightening tool.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
Undo the nuts and remove the connecting rod caps with the half-bearings fitted previously.
1. Use an appropriate graduated measuring tool (1a) to measure the clearance indicated by the plastigage (1b).
| Measurement | Value | Validity |
|---|---|---|
| Clearance between crankpins - crankshaft bearings (mm) | 0.030 ÷ 0.056 | 1.9 JTD 16V |
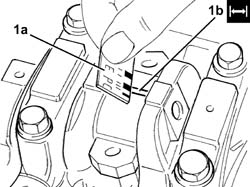
If the value measured is not within the recommended figures, replace the connecting rod bearings.
Carry out this test on all the crankpins, one at a time, without ever turning the crankshaft.
Fit the connecting rod cap complete with half-bearing and secure it without tightening the bolts.
Fit the connecting rods so that the number stamped on each rod faces toward the same side as the number stamped on the big end (inlet side).
- Tighten the connecting rod cap bolts to the recommended torque using the angular tightening tool.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
- Remove the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
Place the crankshaft front cover in its seat complete with gasket and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Crankshaft oil seal cover | Bolt (pretreated to be replaced) | M6 | (engine crankcase side) 0.8 - 1.0 | 1.9 JTD 16v |
- Position the engine oil intake duct in its housing and secure it using the bolts.
1. Place the crankshaft front cover (1a) in its seat using the tool (1b).
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1821247000 | Fitting tool | Fitting crankshaft front oil seal | 1.9 JTD 16V |
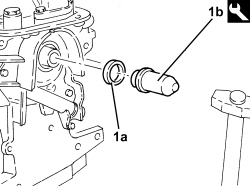
Place the engine rpm sensor in its housing and secure it by tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Rpm sensor | Bolt | M6 | (engine crankcase side) 0.6 - 1.0 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
- Place the timing tensioners support assembly in position and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing tensioners support | Bolt | M10x1.25 | (engine crankcase side) 4.5 - 5.5 | 1.9 JTD 16v 1.9 JTD 8v |
1. Place the flywheel side cover in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Flywheel side oil seal cover | Bolt (pretreated to be replaced) | M6 | (engine crankcase side) 0.8 - 1.0 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
Place the air conditioning compressor mounting (1a) in its housing and secure it tightening the bolts (1b) to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| ACCESSORIES SUPPORT | Bolt | M10 | 4,5 ÷ 5,5 | 1.9 jtd |
- Place the air conditioning compressor in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| COMPRESSOR ON ACCESSORIES MOUNTING | Bolt | M8x1.25x90 | 2,25 ÷ 2,75 |
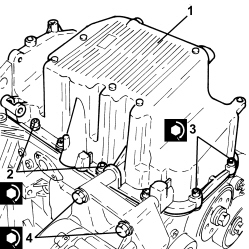
Apply silicon sealant to the entire perimeter of the crankcase sump.
1. Place the crankcase sump in its housing.
2. Tighten the side bolts securing the crankcase sump to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump | Bolt | M8 | (engine crankcase side) 2.3 - 2.8 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
3. Tighten the front and rear bolts securing the crankcase sump to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump | Bolt | M6 | (side and rear) 0.8 - 1.0 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
4. Tighten the bolts securing the air conditioning compressor mounting to the crankcase sump to the recommended torque.
- Fit the flywheel lock.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860846000 | Counter-torque | Flywheel lock |
- Position the toothed timing drive pulley in its housing and secure it tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Toothed drive pulley | Left hand bolt | M16 | (crankshaft side) 32.3 - 35.7 | 1.9 JTD 16v 1.9 JTD 8v |
Remove the flywheel lock.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860846000 | Counter-torque | Flywheel lock |
1. Measure the piston projection in two places at 180° on the gudgeon pin axis using the tool and take the average of the two values measured for each piston.
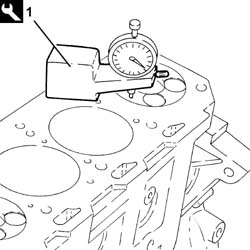
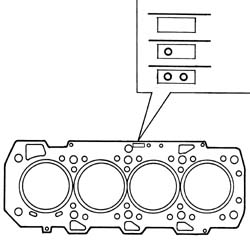
Select the correct size cylinder head gasket depending on the maximum value between of the averages of the projection for each individual piston.
| Measurement | Value | ||
|---|---|---|---|
| Cylinder head gasket size (no hole) (mm) | 0.82 ± 0.05 | ||
| Average - maximum piston projection (mm) | -0.020 ÷ +0.100 | ||
| Measurement | Value | ||
|---|---|---|---|
| Cylinder head gasket size (one hole) (mm) | 0.92 ± 0.05 | ||
| Average - maximum piston projection (mm) | +0.101 ÷ +0.200 | ||
| Measurement | Value | ||
|---|---|---|---|
| Cylinder head gasket size (two holes) (mm) | 1.02 ± 0.05 | ||
| Average - maximum piston projection (mm) | +0.201 ÷ +0.295 | ||
Position the first cylinder at T.D.C.; rotate the crankshaft a further two teeth of the toothed timing drive pulley to lower the pistons thereby preventing any interference with the valves whilst fitting the cylinder head.
- Position the cylinder head locating bushes on the crankcase as shown in the figure.
The locating bushes between the crankcase and cylinder head are shorter (12.5 mm) than the bushes between the cylinder head and the cylinder head extension. Take great care not to reverse them as this could impair engine operation.
Fit the new cylinder head gasket selected.
Position the cylinder head on the cylinder block/crankcase.
Do not reuse the cylinder head bolts more than four times because they undergo permanent lengthening whenever they are tightened.
Replace the bolts if the number of times that the bolts have been tightenened to the cylinder heads is unknown.
1. Tighten the cylinder head bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cylinder head | Bolt | M12 | (engine crankcase side) 6.2 - 6.8 + 90° + 90° + 90° | 1.9 JTD 16v |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860942000 | Torque wrench | Tighten bolts to torque plus angle |
Follow the order shown in the figure for each tightening sequence.
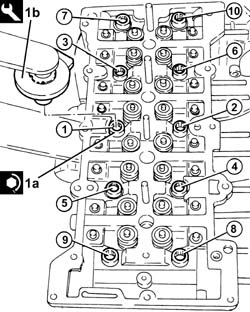
- Refit the glow plugs and tighten them to the recommended torque.
- Fit the pressure pump mounting complete with pressure pump back in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pressure pump mounting | Bolt (pretreated to be replaced) | M8 | (cylinder head extension side) 2.3 - 2.8 | 1.9 JTD 16v |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pressure pump mounting | Bolt (pretreated to be replaced) | M6/M8 | (engine crankcase side) 2.3 - 2.8 | 1.9 JTD 16v |
1. If not already carried out during cylinder head overhaul, remove plugs (1a) and fit camshaft timing adjustment tools (1b) to the cylinder head extension.
Check that the tools are correctly fitted in the housings in the camshafts.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1870896900 | Template | Engine tuning | 1.9 JTD 16V |
Remove the intake camshaft timing tool and tighten the plug.
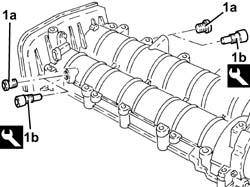
- Place the camshaft housing centering bushes on the cylinder head.
The centering bushes between the cylinder head and the camshaft housing are longer (16.0) than those between the engine block and the cylinder head; take care therefore not to mix them up because this could adversely affect the operation of the engine.
- Place the valve rockers in their housings.
- Place the camshaft housing gasket in position.
- Position the camshaft housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Camshaft housing | Bolt | M8 | (cylinder head side) 2.3 - 2.8 | 1.9 JTD 16v |
If this has not already been done during the overhauling of the cylinder head, loosen the bolt fixing the exhaust side camshaft drive pulley fixing bolt.
1. Undo the bolt fixing the crankcase front cover shown in the diagram.
Temporarily fit the toothed timing drive belt on the drive pulley.
2. Fit the tool.
The crankshaft must be rotated, using small movements, to allow the locating dowel on the timing drive pulley to be inserted in the opening in the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000003000 | Template | Engine tuning | 1.9 JTD 16V 1.9 JTD 8V |
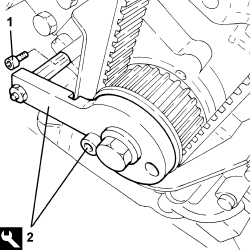
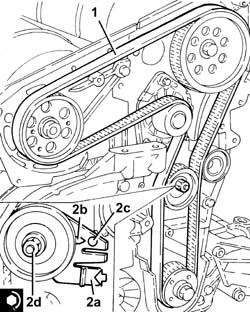
1. Fit the toothed timing belt completely taking care to ensure that the yellow references on it are aligned with the references on the toothed pullies.
2. Use a screwdriver for leverage in the opening (2a) until the reference for the tensioner (2b) is in the maximum tension position and tighten the bolt (2d) for the tensioner to the recommended torque in this position.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing moving tensioner | Nut | M8 | 2.3 ÷ 2.8 | 1.9 JTD 16v 1.9 JTD 8v |
Tighten the bolt fixing the exhaust side camshaft toothed pulley to the recommended torque using the tools for counter-torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Driven toothed pulley | Bolt | M12 | (camshaft side) 2.9 - 3.2 + 40° | 1.9 JTD 16v 1.9 JTD 8v |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1870815000 | Counter-torque | Loosen/tighten timing driven toothed pulley fixing bolt Loosen/tighten nut securing front driveshaft to wheel hub | 1.9 JTD 16V 1.9 JTD 8V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1870836000 | Pins | Loosen/tighten timing driven toothed pulley fixing bolt | 1.9 JTD 16V 1.9 JTD 8V |
Remove the timing tools.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1870896900 | Template | Engine tuning | 1.9 JTD 16V |
Remove the exhaust side camshaft template as the inlet side one has already been removed.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000003000 | Template | Engine tuning | 1.9 JTD 16V 1.9 JTD 8V |
Rotate the crankshaft through two revolutions.
- Loosen the bolt retaining the timing moving tensioner.
- Use a screwdriver for leverage on the tensioner arm until the reference for the tensioner is in line with the reference opening and tighten the tensioner bolt to the recommended torque in this position.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing moving tensioner | Nut | M8 | 2.3 ÷ 2.8 | 1.9 JTD 16v 1.9 JTD 8v |
Recheck the timing by refitting the timing tools.
nly fit the exhaust side camshaft template because the intake side template seat is not accessible.
Tighten the bolt fixing the crankcase front cover removed previously.
Tighten the plug on the cylinder head extension for fitting the exhaust side timing tool.
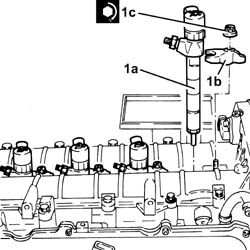
1. Fit the injectors (1a) in their seats complete with brackets (1b) and tighten the nuts (1c) to the recommended torque.
Start the refitting beginning with the injector for cylinder no. 4 and continue with the injectors for cylinders 3, 2, and 1.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Injector brackets | Nut | M8 | (cylinder head extension side) 2.3 - 2.8 | 1.9 JTD 16v 2.4 JTD 20v |
- Place the alternator in position and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| ALTERNATOR TO BRACKET | Bolt | M12 | 6,3 ÷ 7,6 | 1.9 jtd 16v 1.9 jtd 8v 2.4 jtd 20v |
- Place the heat exchanger and engine oil filter mounting in position and secure it using the bolts.
- Fit the pipe from the injectors to the fuel recovery manifold and connect to the fuel recovery manifold.
- Connect the pipe from the injectors to the fuel manifold, injector side pushing it home until the clips click into place.
- Place the single fuel manifold pipe in its housing and secure it by tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Single fuel manifold pipe (rail) | Bolt | M8 | (cylinder head extension side) 2.3 - 2.8 | 1.9 JTD 16v 2.4 JTD 20v |
- Connect the return pipe from the fuel manifold, fuel return manifold side and tighten the band.
- Place the pipe from the pressure pump to the fuel manifold back in its housing and secure it tightening the connectors to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipe from pressure pump to fuel manifold | Connector | M14 | (fuel manifold side) 2.2 - 2.4 | 1.9 JTD 16v 2.4 JTD 20v |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipe from pressure pump to fuel manifold | Connector | M......... | (pressure pump side) ..................... | 1.9 JTD 16v 2.4 JTD 20v |
- Place the pipes from the fuel manifold to the injectors in their housings and secure them tightening the connectors to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipes from fuel manifold to injectors | Connector | M14 | (fuel manifold side) 2.2 - 2.4 | 1.9 JTD 16v 2.4 JTD 20v |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipes from fuel manifold to injectors | Connector | M12 | (injector side) 2.4 - 2.6 | 1.9 JTD 16v 2.4 JTD 20v |
- Place the throttle control shaft valve for the inlet ducts back in its housing and secure it tightening the nuts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Throttle carrier shaft control valve for inlet ducts | Nut | M6 | 0.65 ÷ 0.75 | 1.9 JTD 16v 2.4 JTD 20v |
- Connect the linkage of the intake duct throttle spindle control valve.
- Place the bracket complete with engine oil vapour separator and vacuum reservoir in its housing and secure it using the nuts.
- Connect the engine oil vapour recovery pipes and the engine oil recovery pipe and secure them using the bands.
- Place the vacuum pipes in their housings, connect them and secure them using the bolts.
- Connect the engine oil vapour recovery pipe to the engine oil filler and secure it using the band.
- Place the duplex engine oil heat exchanger rigid supply and return pipe back in its housing, then tighten the bands and the bolts.
- Connect the pipes to the thermostat and tighten the bands.
- Place the exhaust manifold gasket in its housing.
- Place the turbocharger and exhaust manifold assembly complete with catalytic converter back in its housing and secure it tightening the nuts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Turbocharger and exhaust manifold assembly | Nut | M8 | (cylinder head side) 1.8 - 2.2 | 1.9 JTD 16v |
- Connect the engine oil return pipe from the turbocharger, engine crankcase side, and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil supply pipe from turbocharger | Bolt | M8 | (engine crankcase side) 2.2 - 2.7 | 1.9 JTD 16v 1.9 JTD 8v |
Connect the engine oil delivery pipe to turbocharger, engine crankcase side, and tighten the connector to the specified torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil supply pipe to turbocharger | Connector | M12 | (engine crankcase side) 2.2 - 2.7 | 1.9 JTD 16v 1.9 JTD 8v |
- Connect the exhaust gas intake pipe from the exhaust manifold to the E.G.R. heat exchanger, exhaust manifold side, then secure it using the collar and tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Exhaust gas/water heat exchanger for E.G.R. system | Bolt | M8 | (exhaust manifold side) 2.3 - 2.8 | 1.9 JTD 16v 2.4 JTD 20v |
- Place the exhaust manifold heat shield back in its housing and secure it using the nuts.
- Place the engine oil dipstick pipe back in its housing and fasten it with the bolts.
- Place the turbocharger air inlet pipe complete with engine oil vapour recovery pipe in its housing, then secure it using the bands and the bolts.
- Place the power unit timing side rigid support in its housing and secure it by tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing side power unit rigid support | Bolt | M10 | (engine crankcase side) 4.5 - 5.5 | 1.9 JTD 8v 1.9 JTD 16v |
- Position the engine components single belt fixed tensioner in its housing and secure it tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine components single belt fixed tensioner | Bolt | M10x1.5 | (engine crankcase side) 5.0 | 1.9 JTD 16v 1.9 JTD 8v |
- Fit the timing belt covers and secure them using the bolts.
- Position the services pulley in its housing on the crankshaft and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Services pulley on crankshaft | Bolt | M8 | (drive pulley side) 2.3 - 2.8 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
- Adjust the mobile tensioner with a wrench and fit the auxiliary drive belt.
- Connect the electrical connection to the thermal coupling signalling the overheating of the catalytic converter.
- Connect the electrical connection to the air conditioning compressor engagement solenoid.
- Tighten the bolts securing the electrical wiring.
- Connect the electrical connection to the cam angle sensor.
- Connect the electrical connections to the heater plugs.
- Connect the electrical connections to the injectors.
- Connect the electrical connection to the fuel pressure regulator on the injector single manifold.
- Connect the electrical connection to the fuel pressure sensor.
- Connect the electrical connection to the throttle casing.
- Connect the electrical connection to the engine temperature sensor.
- Connect the electrical connection to the fuel pressure regulator.
- Connect the electrical connection to the air temperature and pressure sensor.
- Connect the electrical connection to the E.G.R. solenoid valve.
- Connect the electrical connection to the throttle control shaft valve for the inlet ducts.
- Connect the electrical connection to the engine oil pressure switch.
- Connect the electrical connection to the engine oil level sensor.
- Connect the electrical connection to the rpm sensor.
- Tighten the drain plug in the crankcase sump to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil drain plug | M12x1.25 | (oil sump side) 2.0 | 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
When the refitting of the power unit is completed, refill the engine lubrication system.
Op. 1004D40 ENGINE - POSITION ON STAND AND REMOVE
Removing
Rotate the engine through 180° on the overhaul stand.
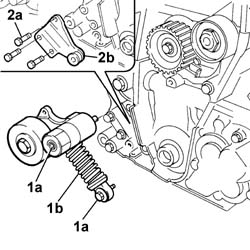
1. Undo the bolts (1a) and remove the automatic engine component single belt tensioner (1b).
2. Undo the fixing bolts (2a) and remove the automatic belt tensioner bracket (2b).
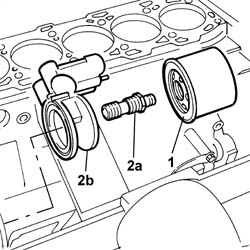
1. Undo and remove the engine oil filter.
2. Undo the centre pin (2a) and remove the engine oil heat exchanger (2b).
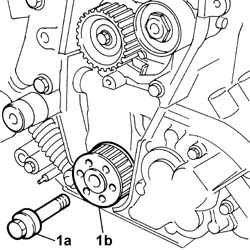
1. Undo the bolt (1a) (left hand thread) and remove the toothed drive pulley (1b).
1. Undo the fixing bolts (1a) and remove the crankshaft front oil seal cover with built-in oil pump (1b).
Remove the seal.
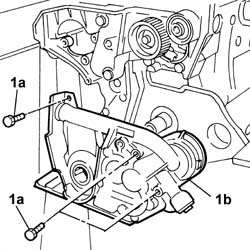
1. Undo the bolt (1a) securing the timing belt tensioner (1b) and remove it.
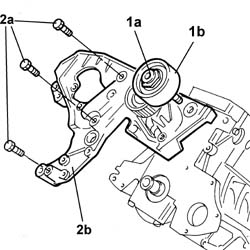
2. Undo retaining bolts (2a) and remove the power steering pump mount, alternator and timing belt tensioner (2b).
Rotate the engine through 180° on the overhaul stand.
1. Fit the tool.
| Description | Code | Function | |
|---|---|---|---|
| 1 | Flange | 1.860.815.000 | Crankshaft rotation |
Rotate the crankshaft using the tool fitted previously until the cylinder concerned is at B.D.C.
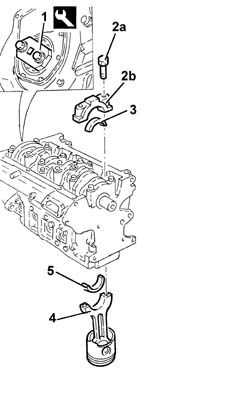
2. Undo the bolts (2a) and remove the connecting rod cap (2b).
3. Remove the lower connecting rod half-bearing.
4. Remove the connecting rod-piston assembly.
5. Remove the upper connecting rod half-bearing.
Carry out the same operations to remove the pistons and connecting rods for the remaining cylinders.
Check that the crankshaft endfloat corresponds to the recommended figures using a magnetic base and dial gauge.
| Subject | Value | |
|---|---|---|
| Crankshaft | mm | |
| End float |
If the value for the crankshaft endfloat does not correspond with the recommended figures, when refitting, regrind the crankcase seat and use suitable oversize thrust washers.
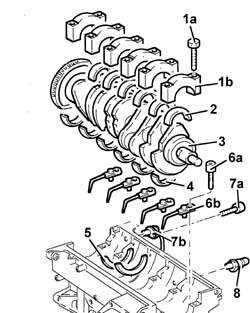
1. Undo the bolts (1a) and remove the connecting rod caps (1b).
2. Remove the lower main journal half-bearings.
3. Remove the crankshaft.
4. Remove the upper main journal half-bearings.
5. Remove the thrust washers.
6. Undo the bolts (6a) and remove the jets (6b) from the crankcase.
7. Undo the bolt (7a) and remove the rpm and timing sensor (7b).
8. Remove the engine oil minimum pressure warning light sensor.
. Remove the engine block from the overhaul stand and place on a work bench.
Undo the bolts and remove the intake duct from the oil pump.
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
Drill and remove the water/oil sealing plugs from the crankcase to allow for washing.
Refitting
Wash the dismantled components.
Fit the water/oil sealing plugs in the crankcase using suitable fitting tools.
Lubricate all the mechanical components with engine oil.
Check that the cylinder head support surface does not have cracks or superficial grooves.
Check that the planarity of the cylinder head support surface corresponds to the recommended figure; if this is not the case, regrind the cylinder head support surface.
| Subject | Value | |
|---|---|---|
| Cylinder block/crankcase | mm | |
| Cylinder head support surface flatness | < 0.1 |
1. Measure the cylinder bore diameter using the diagram illustrated.
| Subject | Value | ||
|---|---|---|---|
| 1 | Cylinder block/crankcase | mm | |
| Cylinder liner bore | 82.000 - 82.010 | ||
| 82.010 - 82.020 | |||
| 82.020 - 82.030 |
Check that the taper of the cylinder liners is within the recommended limits.
| Subject | Value | |
|---|---|---|
| Cylinder block/crankcase | mm | |
| Cylinder liner taper | < 0.005 |
Check that the ovality of the cylinder liners is within the recommended limits.
| Subject | Value | |
|---|---|---|
| Cylinder block/crankcase | mm | |
| Cylinder liner ovality | < 0.05 |
If the cylinder bore measurements are not within the recommended limits, ream the cylinder bores following the recommended oversizes.
In the case of reaming, all the bores must have the same oversize.
| Subject | Value | |
|---|---|---|
| Cylinder block/crankcase | mm | |
| Cylinder liner oversize | 0.1 |
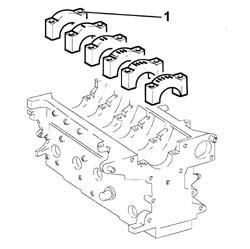
1. Fit the bearing caps.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
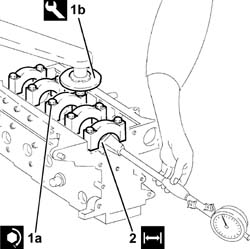
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1a | (engine crankcase side) 2.5 + 100° | Bolt | MAIN BEARING CAPS | M12 |
| Description | Code | Function | |
|---|---|---|---|
| 1b | Torque wrench | 1.860.942.000 | Angular tightening of bearing cap bolts |
2. Check that the diameter of the main journal seats is within specified limits.
| Subject | Value | |
|---|---|---|
| 2 | Bearing caps | mm |
| Main journal seat diameter | 63.705 ÷ 63.718 |
Check that there are no deposits or blockages in the crankshaft lubrication ducts.
Check that the diameter of the main journals is within specified limits.
| Subject | Value | |
|---|---|---|
| Crankshaft | mm | |
| Main journal diameter - Category A | 59.994 ÷ 60.000 | |
| Category B | 59.988 ÷ 59.994 | |
| Category C | 59.982 ÷ 59.988 |
If the diameter of the main journals is not correct, they should be reground to the recommended undersize.
| Subject | Value | |
|---|---|---|
| Crankshaft | mm | |
| Main journal undersize | 0.127 |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept.
Check that the diameter of the crankpins corresponds to the recommended figures.
| Subject | Value | |
|---|---|---|
| Crankshaft | mm | |
| Crankpin diameter - Category A | 50.799 ÷ 50.805 | |
| Category B | 50.793 ÷ 50.799 | |
| Category C | 50.787 ÷ 50.793 |
If the diameter of the crankpins is not correct, they should be reground to the recommended undersize.
| Subject | Value | |
|---|---|---|
| Crankshaft | mm | |
| Main journal undersize | 0.127 |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept.
Check that the small end bush internal diameter is within the recommended limits; if not, replace the worn small end bush (Ref. op. 1028H58).
| Subject | Value | |
|---|---|---|
| Small end bush | mm | |
| Inner diameter | 26.006 - 26.014 |
Check that the inner diameter of the piston bushes corresponds to the recommended figures; if not, replace the piston complete with piston rings, gudgeon pin and bushes.
| Subject | Value | |
|---|---|---|
| Pistons | mm | |
| Piston bush internal diameter | 25.999 ÷ 26.004 |
Check that the outer diameter of the gudgeon pins is within the recommended limits; if not, replace the worn gudgeon pins.
| Subject | Value | |
|---|---|---|
| Gudgeon pins | mm | |
| Outer diameter | 25.982 ÷ 25.987 |
Fit the piston rings in the cylinder liner and check that the opening between the ends is within the recommended values; if this is not the case, replace the circlips.
| Subject | Value | |
|---|---|---|
| Piston rings | mm | |
| 1st piston ring gap | 0.20 ÷ 0.35 | |
| 2nd piston ring gap | - ÷ - |
| Subject | Value | |
|---|---|---|
| Oil scaper ring | mm | |
| Oil scraper ring gap | - ÷ - |
Check that the outer diameter of the pistons is within specified limits; if not, replace the piston complete with sealing rings and pin.
| Subject | Value | |
|---|---|---|
| Pistons | mm | |
| Outer diameter - Category A | 81.920 ÷ 81.930 | |
| Category B | 81.930 ÷ 81.940 | |
| Category C | 81.940 ÷ 81.950 |
Measure perpendicular to the gudgeon pin axis, 9 mm from the lower edge of the skirt.
1. Check that the axial clearance (1a) between the second ring (1b) and the housing in the piston (1c) corresponds to the recommeded figure.
| Subject | Value | |
|---|---|---|
| 1a | Piston rings | mm |
| End float | - ÷ - |
Check that the axial clearance between the oil scraper ring and the housing in the piston corresponds to the recommeded figures.
| Subject | Value | |
|---|---|---|
| Oil scaper ring | mm | |
| End float |
1. Fit the caps (1b) on the connecting rods (1a) and secure them tightening the bolts (1c) to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1c | 2.5 + 60° | CONNECTING ROD CAPS | M9 |
Use the special tool for the angular tightening of the connecting rod cap bolts.
| Description | Code | Function | |
|---|---|---|---|
| Torque wrench | 1.860.942.000 | Angular tightening of bearing cap bolts |
2. - Check that the diameter of the big end corresponds to the recommended figures; if not, replace the connecting rods.
| Subject | Value | |
|---|---|---|
| 2 | Connecting rods | mm |
| Big end diameter | 53.897 ÷ 53.909 |
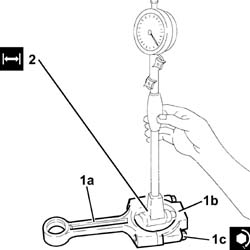
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
Check that there are no signs of seizing on the flywheel ring gear teeth; if this is not the case, replace it.
Fit the crankcase on the overhaul stand and secure it using the bolts.
Fit the minimum engine oil pressure warning light sensor and tighten it to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.7 ÷ 4.0 | MINIMUMM ENGINE OIL PRESSURE WARNING LIGHT SENSOR |
Fit the thrust washers on the fourth bearing support.
The crankshaft supplied by the Parts Dept. comes without half-bearings and the main journals and crankpins are the "normal" size; the half-bearings to be fitted must therefore be selected identifying the class of each main journal and crankpin for the new crankshaft.
The following must be determined for the selection of main journal half-bearings:
- the numerical code stamped on the flywheel;
- the paint mark, if present, next to the main journals.
Below is an example of the identification of main journal grades.
1. - Crankpin identification numerical code: the number on the left refers to the first timing side bearing; for 4 cylinder engines, there is an "N" in place of the number for the 5th bearing
2. - Main journal identification numerical code: the first number on the left refers to the first timing side bearing; for 4 cylinder engines, there is an "N" in place of the number for the 6th bearing
3. - Series of numbers (if present), in groups of two digits, which indicate the dimensions (thousandth part) of the main journals: the first two numbers on the left refer to the first timing side bearing
Only use the codes that relate to the key, all other codes on the flywheel should not be used.
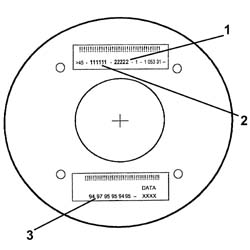
For the identification of the main journal grade, refer to the numerical code for reference 2.
In the case of the example, the numbers 111111 indicate that all six bearings are Grade A (red) as indicated in the Table.
A further method for identifying the grade of the bearings is to read reference 3 (if present) in the diagram.
In the case of the example, the number 94 (first on the left) corresponds to the dimensions 59.994 for the first timing side bearing which, as indicated in the Table, identifies Grade A (red); the same method should be applied for other groups of two digits for the same reference 3 (97 - 95 - 95 - 94 - 95).
Bearing grade A - Normal, diameter (mm) 59.994 - 60.000, paint mark, numerical code 1 (94 00)°
Bearing grade B - Normal, diameter (mm) 59.987 - 59.993, paint mark, numerical code 2 (88 94)°
Bearing grade C - Normal, diameter (mm) 59.982 - 59.986, paint mark, numerical code 3 (82 88)°
Bearing grade D - Undersize, diameter (mm) 59.867 - 59.873, paint mark, numerical code 6 (67 73)°
Bearing grade E - Undersize, diameter (mm) 61 - 59.866, paint mark, numerical code 7 (60 67)°
Bearing grade F - Undersize, diameter (mm) 55.885 - 59.859, paint mark, numerical code 8 (55 61)°
(*) 0.127 mm undersize
(°) Last two numbers (thousandth part) of the main journal dimensions
In the case of the usage of a crankshaft where the maximum undersize for the bearings is 0.127 mm through grindings, the grade should be selected through the measurement of the diameter of the bearing using the Table as a reference.
Having defined the grade and the colour of each new or reground crankshaft bearings, it is necessary to select the thickness of the bearings that should be the same colour as the corresponding bearing; the pair of half-bearings required can be ordered from the Parts Dept. by quoting the order no.
The above is designed to guarantee the optimum operational clearances for all the bearings.
Lastly, we wish to point out that, generally, the clearance between the main journal and the half-bearing, obtained through the selection method indicated above, should be within the following values:
- Minimum: - - Maximum: -; this value can be measured, as a final check, using the calibrated wire (plastic gauge).
1. Fit the bolts (1a) and fasten the jets (1b) to the crankcase at the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1a | 0.9 - 1.2 | Bolt | PISTON COOLING NOZZLES |
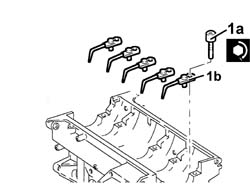
Fit the main journal half-bearings in the cylinder block/crankcase.
Fit the crankshaft in the crankcase.
1. Fit the main bearing caps complete with half-bearings.
The bearing caps have progressively numbered references (from zero to five starting from the engine pulley side) which define the fitting position.
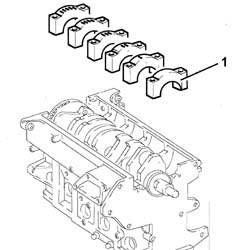
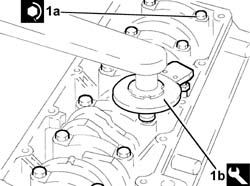
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1a | 2.5 + 100° | Bolt | MAIN BEARING CAPS | M12 |
| Description | Code | Function | |
|---|---|---|---|
| 1b | Torque wrench | 1.860.942.000 | Angular tightening of bearing cap bolts |
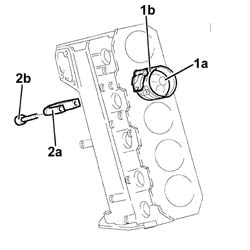
Fit the tool.
| Description | Code | Function | |
|---|---|---|---|
| Flange | 1.860.815.000 | Crankshaft rotation |
Rotate the crankcase through 90° on the overhaul stand.
Rotate the crankshaft using the tool fitted previously until the cylinder concerned is at B.D.C.
1. Fit the piston-connecting rod assembly (1a) complete with half-bearing using the tool (1b).
The piston-connecting rod assemblies are fitted in the cylinder block/crankcase so that the combustion chamber in the piston is facing the intake side.
For the selection of the connecting rod half-bearings, follow the procedure described previously for the main journal half-bearings.
2. Fit the connecting rod cap (2a) complete with half-bearing and secure it without tightening the bolts (2b).
Fit the connecting rods so that the number stamped on each rod faces toward the same side as the number stamped on the big end (inlet side).
Carry out the same operations to refit the pistons and connecting rods for the remaining cylinders.
Rotate the crankcase through 90° on the overhaul stand.
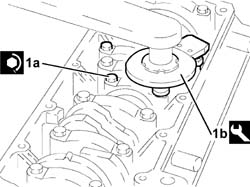
1. Tighten the connecting rod cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1a | 2.5 + 60° | Bolt | CONNECTING ROD CAPS | M9 |
| Description | Code | Function | |
|---|---|---|---|
| 1b | Torque wrench | 1.860.942.000 | Angular tightening of bearing cap bolts |
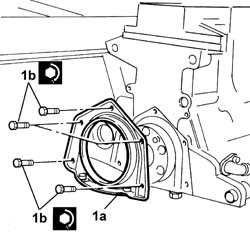
1. Fit the crankcase rear cover (1a) with the oil seal incorporated and tighten bolts (1b) to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1b | 0.9 - 1.2 | Bolt | CRANKCASE REAR COVER | M6 |
Rotate the crankshaft so that cylinder no. 1 is at T.D.C.
Fit the front crankcase cover with oil pump complete with gasket
Tighten the crankcase front cover bolts, complete with oil pump, to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 0.9 - 1.3 | Bolt | FRONT COVER CRANKCASE COMPLETE WITH OIL PUMP | M6 |
Fit the engine oil intake complete with O-Ring and secure it using the bolts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 0.9 - 1.3 | OIL SECTION PUMP |
Apply the recommended sealant to the entire perimeter of the crankcase sump.
| Description | Q.ty | Component | Type | Classification | |
|---|---|---|---|---|---|
| Dow corning 7091 | ENGINE OIL SUMP | Silicon sealant |
1. Fit the crankcase sump.
2. Tighten the side bolts (2a) fixing the crankcase sump to the recommended torque using the tool (2b).
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2a | (engine crankcase side) 0.9 - 1.2 | Side bolts | CRANKCASE SUMP | M6 |
| Description | Code | Function | |
|---|---|---|---|
| 2b | Spanner | 1.860.834.001 | Loosen/Tighten crankcase sump side bolts |
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2a | (engine crankcase side) 2.1 - 2.6 | Front and rear bolts | CRANKCASE SUMP | M8 |
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2a | (engine crankcase side) 2.3 - 3.3 | Front and rear bolts | CRANKCASE SUMP | M8 |
| Description | Code | Function | |
|---|---|---|---|
| 2b | Spanner | 1.860.833.001 | Loosen/Tighten front and rear crankcase sump bolts |
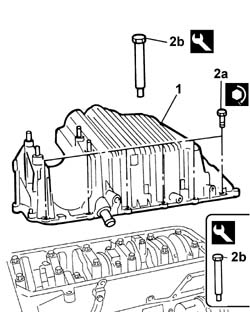
Rotate the engine through 180° on the overhaul stand.
Fit the flywheel lock.
| Description | Code | Function | |
|---|---|---|---|
| Counter-torque | 1.860.846.000 | Flywheel lock |
Fit the flywheel and tighten the bolts to the recommended torque with loctite.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (crankshaft side) 14.7 - 21.2 | Bolt with thread-locking agent | ENGINE FLYWHEEL | M12 |
Fit the toothed drive pulley for the timing belt and tighten the (left hand thread) bolt to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (crankshaft side) 32.9 - 44.1 | Bolt (left hand thread) | TOOTHED DRIVE PULLEY | M16 |
Remove the tool.
| Description | Code | Function | |
|---|---|---|---|
| Counter-torque | 1.860.846.000 | Flywheel lock |
1. Measure the piston projection in two places at 180° on the gudgeon pin axis using the tool and take the average of the two values measured for each piston.
| Description | Code | Function | |
|---|---|---|---|
| 1 | Dial gauge support | 1.870.404.000 | Piston projection from cylinder head support plane check |
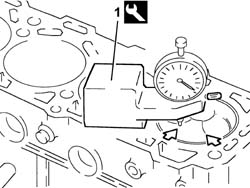
Select the correct size cylinder head gasket depending on the maximum average protrusions for each individual piston.
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Shim (no reference) | 0.82 |
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Average maximum piston projection | 0.201 ÷ 0.295 |
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Shim (two references) | 1.02 |
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Average maximum piston projection | 0.101 ÷ 0.200 |
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Shim (one reference) | 0.92 |
| Subject | Value | |
|---|---|---|
| Cylinder head gasket | mm | |
| Average maximum piston projection | 0.020 ÷ 0.100 |
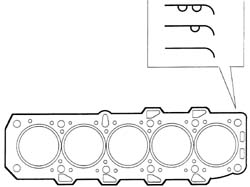
Position the cylinder head locating bushes on the engine block.
Fit the cylinder head gasket selected.
The cylinder head gasket is ASTADUR type. The material from which the gasket is made undergoes a polymerization process during the operation of the engine so that it becomes considerably harder during usage.
In order for the polymerization process to take place, it is necessary to:
Position the cylinder head on the cylinder block/crankcase.
1. Tighten the cylinder head bolts (1a) to the recommended torque using the angular tightening tool (1b).
Follow the order shown in the figure for each tightening sequence.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 1a | 2 + 6.5 + 90° + 90° + 90° | Bolts | CYLINDER HEAD | M12 |
The figure of 2 daNm in the table below is a tightening value for all the bolts following the order illustrated in the diagram.
| Description | Code | Function | |
|---|---|---|---|
| 1b | Torque wrench | 1.860.942.000 | Cylinder head bolts angular tightening |
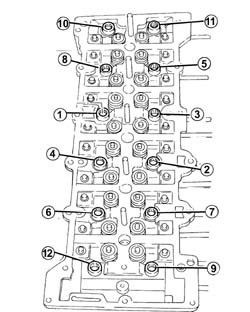
Fit the cam cover complete with gasket and secure it by tightening the bolts to torque.
Fit the alternator mount, power steering pump and timing belt tensioner and tighten the bolts.
Fit the fixed timing belt tensioner and tighten the retaining bolt to torque.
Fit the water/oil heat exchanger and tighten the threaded fitting.
Tighten the engine oil filter cartridge.
Fit the single engine component drivebelt automatic tensioner bracket and tighten the bolts.
Fit the automtic belt tensioner and tighten the fixing bolts.
1. Remove plug (1a) and fit camshaft timing tools (1b) to the cylinder head extension.
Check the tools marked "A" are correctly fitted in the seats on the camshafts.
| Description | Code | Function | |
|---|---|---|---|
| 1b | Templates | 1.870.986.900 | Engine tuning |
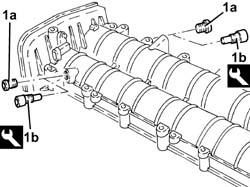
1. Position the cylinder head extension assembly (1a) in its housing and secure it by tightening the bolt (1b) to the recommended torque.
2. Tighten the fixing bolts to the recommended torque.
Loosen the bolt securing the exhaust side timing belt toothed drive pulley.
Remove the intake camshaft timing tool and tighten the plug.
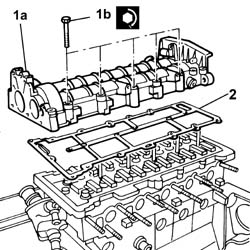
1. Undo the bolt fixing the crankcase front cover shown in the diagram.
Temporarily fit the toothed timing drive belt on the drive pulley.
2. Fit the tool (2a) and fasten it using the calibrated screw (2b).
The crankshaft must be rotated, using small movements, to allow the locating dowel on the timing drive pulley to be inserted in the opening in the tool.
| Description | Code | Function | |
|---|---|---|---|
| 2a | Template | 1.860.905.000 | Engine tuning |
| Description | Code | Function | |
|---|---|---|---|
| 2b | Calibrated screw | 1.860.905.010 | Engine tuning |
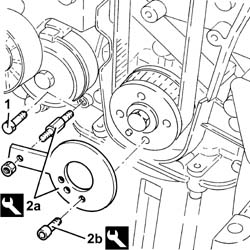
Position the engine oil filler fitting metal gasket.
Place the engine oil filler fitting in position and tighten the fixing bolts.
Positon the vacuum pump metal gasket.
Fit the vacuum pump in place and tighten the bolts.
Fit the glow plugs.
Fit the cooling system rigid pipe gasket.
Place the rigid cooling system pipe in position and tighten the fixing bolts.
Place the EGR heat exchanger in position and tighten the fixing bolts.
Fit the pipes on the EGR heat exchanger and renew the fastening bands.
Positon the intake manifold metal gasket.
Place the intake manifold in position and tighten the fixing nuts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.5 | Nut | INLET MANIFOLD | M8 |
Place the rigid EGR pipe in position and tighten the fixing bolts.
Fit the power steering pump in position.
Place the pressure pump mount in position and tighten the fixing bolts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (Cylinder block/crankcase) 2.5 | Bolt | INJECTION PRESSURE PUMP MOUNT | M8 |
Tighten the bolts fixing the power steering pump.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.5 | Bolt | POWER STEERING PUMP | M8 |
Place the pressure pump in position and tighten the fixing nuts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.5 | Nut | PRESSURE PUMP | M8 |
Fit the pressure pump pulley.
Lock the rotation of the pressure pump drive pulley using two bolts.
Tighten the pressure pump drive pulley nut.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 5 | Nut | PRESSURE PUMP CONTROL PULLEY | M14 |
Undo the two bolts for locking the rotation of the pressure pump drive pulley fitted previously.
1. Fully fit the toothed timing drive belt.
2. Use a screwdriver for leverage in the opening (2a) until the reference for the tensioner (2b) is aligned with the opening reference (2c) and, in this position, tighten the nut (2d) for the belt tensioner to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2d | 2.5 | Nut | MOBILE TIMING TENSIONER | M8 |
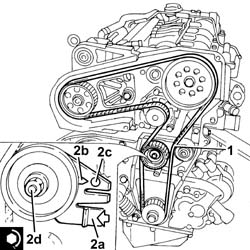
Tighten the bolt fixing the exhaust side camshaft toothed pulley to the recommended torque.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 12 | Bolt | TIMING DRIVEN PULLIES | M12 |
Remove the timing tools.
| Description | Code | Function | |
|---|---|---|---|
| Templates | 1.870.986.900 | Engine tuning |
Remove the exhaust side camshaft template as the inlet side one has already been removed.
| Description | Code | Function | |
|---|---|---|---|
| Template | 1.860.905.000 | Engine tuning |
| Description | Code | Function | |
|---|---|---|---|
| Calibrated screw | 1.860.905.010 | Engine tuning |
Rotate the crankshaft through two revolutions.
Recheck the timing by refitting the timing tools.
Only fit the exhaust side camshaft template because the intake side template seat is not accessible.
Check the timing belt tensioner references are aligned.
Tighten the bolt fixing the crankcase front cover removed previously.
Tighten the plug on the cylinder head extension for fitting the exhaust side timing tool.
Fit the injectors and brackets in their seats and tighten the nuts.
Begin to fit, starting from the injector for the cylinder 5, followed by cylinders 4, 3, 2, 1.
Fit the rigid fuel pipe to the pump and tighten the fastening.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (pump side) 2.3 | Connector | PRESSURE PUMP LINE TO FUEL MANIFOLD | M14X1.5 |
Fit the fuel vapour recovery tank and tighten the bolts, connect the pipes to the pressure pump and injectors.
Position the oil vapour recovery tank and tighten the bolt.
Fit the oil vapour recovery pipes in their seats on the engine oil sump, cylinder heads and engine block and restore the fastening collars.
Position the engine oil dipstick, then tighten the fastening.
Place the rigid cooling system pipe in position and tighten the fixing bolts, connect the pipes and renew the fastening bands.
Place the single fuel pipe in position and tighten the fixing bolts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.5 | Bolts | INJECTOR FUEL MANIFOLD (DIESEL) | M8 |
Fit new rigid fuel pipes from the single fuel pipe to the injectors and tighten the connectors.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (injector side) 2 | Connectors | INJECTOR FUEL MANIFOLD PIPE | M12X1.5 |
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (manifold side) 2 | Connectors | PIPE FUEL MANIFOLD TO INJECTORS | M12X1.5 |
Clean the threaded pipe seats on the manifold and injectors with heptane.
Tighten the pressure pump rigid fuel pipe to the single fuel pipe.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| (manifold side) 2.3 | Connector | PRESSURE PUMP LINE TO FUEL MANIFOLD | M14X1.5 |
Fit the rigid pipe and tighten the fixing bolts.
Fit the toothed drive belt protective covers and tighten the bolts.
Position the flywheel retaining tool in its seat.
| Description | Code | Function | |
|---|---|---|---|
| Flywheel lock | 1.860.846.001 | Prevent the rotation of the crankshaft |
Fit the crankshaft pulley in position and tighten the fixing bolts.
| Value daNm | Fastening | Component | Ø | |
|---|---|---|---|---|
| 2.5 | Bolt | CRANKSHAFT PULLEY | M8 |
Fit the fixed timing belt tensioner for the single engine component drive belt and tighten the retaining bolt to torque.
Remove the flywheel retainer.
| Description | Code | Function | |
|---|---|---|---|
| Flywheel lock | 1.860.846.001 | Prevent the rotation of the crankshaft |
Fit the engine wiring with ducts and tighten the bolts.
Connect the electrical connection for the timing sensor.
| Description | Connector | |
|---|---|---|
| Timing sensor | K047 |
Connect the electrical connections for the injectors.
| Description | Connector | |
|---|---|---|
| Injector | N070A |
| Description | Connector | |
|---|---|---|
| Injector | N070E |
| Description | Connector | |
|---|---|---|
| Injector | N070D |
| Description | Connector | |
|---|---|---|
| Injector | N070C |
| Description | Connector | |
|---|---|---|
| Injector | N070B |
Connect the glow plug electrical connections.
| Description | Connector | |
|---|---|---|
| Heater plugs | A040A |
| Description | Connector | |
|---|---|---|
| Heater plugs | A040E |
| Description | Connector | |
|---|---|---|
| Heater plugs | A040D |
| Description | Connector | |
|---|---|---|
| Heater plugs | A040C |
| Description | Connector | |
|---|---|---|
| Heater plugs | A040B |
Connect the electrical connection for the turbo sensor.
| Description | Connector | |
|---|---|---|
| Supercharging sensor | K082 |
Connect the electrical connection for the fuel pressure regulator.
| Description | Connector | |
|---|---|---|
| Fuel pressure regulator | N077 |
Connect the electrical connection for the fuel pressure sensor.
| Description | Connector | |
|---|---|---|
| 3 | Fuel pressure sensor | K083 |
Connect the electrical connection for the EGR solenoid valve.
| Description | Connector | |
|---|---|---|
| EGR solenoid valve | L030 |
Connect the electrical connection for the engine rpm sensor.
| Description | Connector | |
|---|---|---|
| Rpm sensor | K046 |
Connect the electrical connection for the coolant temperature sensor.
| Description | Connector | |
|---|---|---|
| Engine coolant temperature sensor/sender unit | K036 |
Op. 1004D40 ENGINE - POSITION ON STAND AND REMOVE
Removing
1. Fit the tool on the crankshaft.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
2. Lock the crankshaft using the tool fitted previously for undoing the (left) bolt (2a) and remove the toothed drive pulley (2b).
3. Undo the bolts (3a), (3b) and remove the crankcase front cover with the oil pump incorporated (3c) complete with intake (3d).
4. Undo the bolts and remove the support (4a) complete with moving timing belt tensioner (4b).
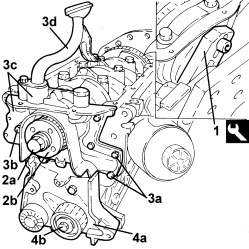
1. Undo the bolts (1a) and remove the engine oil filter mounting (1b) complete with heat exchanger (1c).
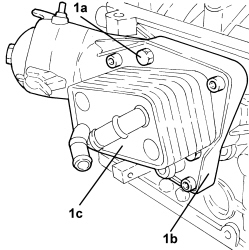
1. Undo the bolts (1a) and remove the connecting rod cap (1b).
2. Remove the lower connecting rod half-bearing.
3. Remove the connecting rod-piston assembly
4. Remove the upper connecting rod half-bearing.
- Carry out the same operations to remove the pistons and connecting rods for the remaining cylinders.
- Remove the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
5. Undo the bolts (5a) and remove the crankcase rear cover (5b) with the oil seal incorporated.
- Check that the crankshaft endfloat corresponds to the recommended figures using a magnetic base and dial gauge.
| Measurement | Value | Validity |
|---|---|---|
| Crankshaft endfloat | 0.049 - 0.211 mm | 1.9 JTD 16V |
- If the value for the crankshaft endfloat does not correspond with the recommended figures, when refitting, regrind the crankcase seat and use suitable oversize thrust washers.
6. Undo the bolts (6a) and remove the bearing caps (6b).
7. Remove the lower main journal half-bearings.
8. Remove the crankshaft.
9. Remove the upper main journal half-bearings.
10. Remove the thrust washers.
11. Undo the bolts (11a) and remove the jets (11b) from the crankcase.
12. Undo the bolt (12a) and remove the rpm sensor (12b).
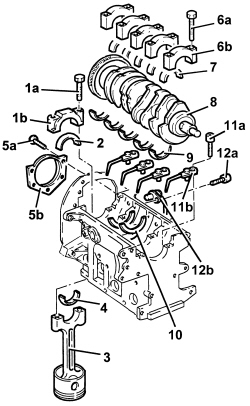
- Rotate the crankcase through 90° on the overhaul stand.
- Undo the bolts and remove the crankcase from the mounting, then place it on a special workbench.
- Undo the bolts and remove the intake duct from the oil pump.
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
Refitting
- Wash the dismantled components.
- Fit the water/oil sealing plugs in the crankcase using suitable fitting tools.
- Lubricate all the mechanical components with engine oil.
- Check that the cylinder head support surface does not have cracks or superficial grooves.
- Check that the planarity of the cylinder head support surface corresponds to the recommended figure; if this is not the case, regrind the cylinder head support surface.
| Measurement | Value | Validity | ||
|---|---|---|---|---|
| Cylinder head support surface flatness | <0.1 mm | 1.9 JTD 8V 1.9 JTD 16V | ||
1. Measure the cylinder bore diameter using the diagram illustrated.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade A | 82.000 - 82.010 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade B | 82.010 - 82.020 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade C | 82.020 - 82.030 mm | 1.9 JTD 8V 1.9 JTD 16V |
- Check that the taper of the cylinder liners/bores is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner taper | <0.005 mm | 1.9 JTD 8V 1.9 JTD 16V |
- Check that the ovality of the cylinder liners is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner ovality | <0.05 mm | 1.9 JTD 8V 1.9 JTD 16V |
1. If the cylinder bore measurements are not within the recommended limits, ream the cylinder bores following the recommended oversizes.
In the case of reaming, all the bores must have the same oversize.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner bore diameter oversize | 0.1 mm | 1.9 JTD 8V 1.9 JTD 16V |
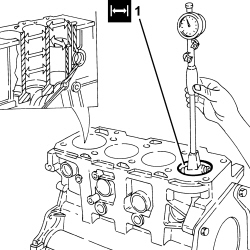
1. Temporarily fit the bearing caps.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
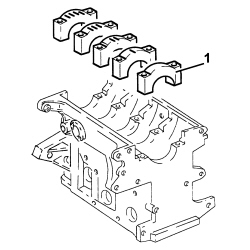
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 2.4 ÷ 2.6 + 100° | 1.9 JTD 8V |
2. Check that the diameter of the main journal seats is within specified limits.
| Measurement | Value | Validity |
|---|---|---|
| Main journal seat diameter | 63.705 - 63.718 mm | 1.9 JTD 8V 1.9 JTD 16V |
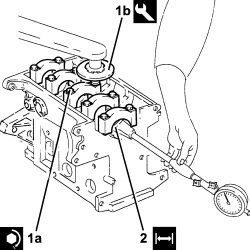
- Check that there are no deposits or blockages in the crankshaft lubrication ducts.
- Check that the diameter of the main journals corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category A | 59.994 - 60.000 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category B | 59.987 - 59.993 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter - Category C | 59.982 - 59.986 mm | 1.9 JTD 8V |
- If the diameter of the main journals is not correct, they should be reground to the recommended undersize.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter oversize | 0.127 mm | 1.9 JTD 8V |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept. The half-bearings used for undersizes of more than 0.127 mm should not be ordered from the Parts Dept. (even if the number is still quoted).
- Check that the diameter of the crankpins corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category A | 50.799 - 50.805 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category B | 50.793 - 50.799 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter - Category C | 50.787 - 50.793 mm | 1.9 JTD 8V 1.9 JTD 16V |
- If the diameter of the crankpins is not correct, they should be reground to the recommended undersize.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter undersize | 0.127 mm | 1.9 JTD 8V 1.9 JTD 16V |
Crankpin undersizes higher than the value mentioned will adversely affect the structural resistance of the crankshaft (following contact between the tool and rolled connectors). As far as the above is concerned, if the regrinding requires undersizes greater than 0.127 mm, then the crankshaft must be replaced and a new one ordered from the Parts Dept. The half-bearings used for undersizes of more than 0.127 mm should not be ordered from the Parts Dept. (even if the number is still quoted).
- Check the main bearings, noting that the half-bearings should not be adapted. Replace them if scoring or signs of binding are noted.
- Fit the half-bearings making sure they are scrupulously clean.
If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
- Fit the crankshaft into its seat on the crankcase.
1. Fit the calibrated wire (plastigage) for measuring the bearing clearance.
Check one journal at a time, without rotating the crankshaft.
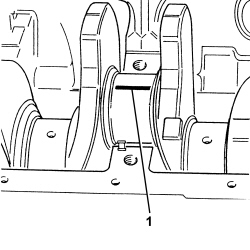
1. Fit the main bearing caps complete with half-bearings.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
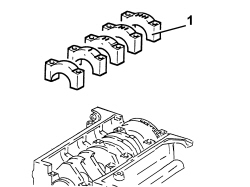
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 2.4 ÷ 2.6 + 100° | 1.9 JTD 8V |
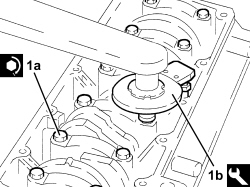
1. Remove the bearing caps fitted previously and, using a suitable graduated measuring instrument (1a), measure the clearance shown by the calibrated wire (1b).
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main journals - crankshaft bearings | 0.011 - 0.071 mm | 1.9 JTD 8V 1.9 JTD 16V |
If the figure measured is outside of the tolerance, replace the half-bearings with ones of the correct size and category.
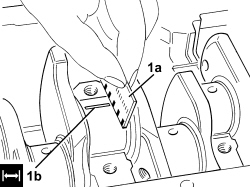
- Measure the clearance for all the bearings taking care to take the measurements one at a time without moving the crankshaft at any time.
- Check that the small end bush internal diameter is within the recommended limits; if not, replace the worn small end bush.
Op. 1028H58 CONNECTING ROD SMALL END BUSH (ONE) - REPLACE
| Measurement | Value | Validity |
|---|---|---|
| Small end bush inner diameter | 26.006 - 26.012 mm | 1.9 JTD 8V |
- Check that the diameter of the gudgeon pin housing corresponds to the recommended figures; if not, replace the piston complete with piston rings, gudgeon pin and bushes.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin housing diameter in piston | 25.999 - 26.004 mm | 1.9 JTD 8V 1.9 JTD 16V |
- Check that the outer diameter of the piston pins is within the recommended limits; if not, replace the worn piston pins.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin outer diameter | 25.982 - 25.987 mm | 1.9 JTD 8V 1.9 JTD 16V |
- Fit the piston rings in the cylinder bore and check that the opening between the ends is within the recommended values; if this is not the case, replace the circlips.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring gap | 0.20 - 0.35 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring gap | 0.25 - 0.50 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring gap | 0.25 - 0.50 mm | 1.9 JTD 8V |
- Check that the piston ring seat is within the recommended values.
| Measurement | Value | Validity |
|---|---|---|
| Piston ring seat in piston - 1st groove | 2.080 ÷ 2.100 | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Piston ring seat in piston - 2nd groove | 2.020 ÷ 2.040 | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Piston ring seat in piston - 3rd groove | 2.020 ÷ 2.040 | 1.9 JTD 8V |
- Check that the thickness of the piston rings is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring thickness | 1.970 - 1.995 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring thickness | 1.970 - 1.995 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring thickness | 1.970 - 1.990 mm | 1.9 JTD 8V |
- Check that the outer diameter of the pistons corresponds to the recommended figures; if not, replace the piston complete with piston rings and gudgeon pin.
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - Grade A | 81.920 - 81.930 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - Grade B | 81.930 - 81.940 mm | 1.9 JTD 8V 1.9 JTD 16V |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - Grade C | 81.940 - 81.950 mm | 1.9 JTD 8V 1.9 JTD 16V |
Measure perpendicular to the gudgeon pin axis, 8 mm from the lower edge of the skirt.
- Check that the axial clearance between the pistons rings and the seats corresponds to the recommeded figures.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring endfloat | 0.085 - 0.130 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring endfloat | 0.025 - 0.070 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Engine piston oil scraper ring endfloat | 0.030 - 0.070 mm | 1.9 JTD 8V |
1. Fit the caps (1b) on the connecting rods (1a) and secure them tightening the bolts (1c) to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
- Use the tool for the angular tightening of the connecting rod cap bolts.
2. - Check that the diameter of the big end corresponds to the recommended figures; if not, replace the connecting rods.
| Measurement | Value | Validity |
|---|---|---|
| Big end inner diameter | 53.897 - 53.909 mm | 1.9 JTD 8V 1.9 JTD 16V |
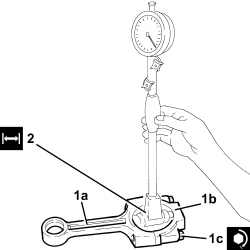
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
- Fit the intake duct on the oil pump and secure it using the bolts.
- Fit the crankcase on the overhaul stand and secure it using the bolts.
- Position the rpm sensor in its housing and secure it using the bolt.
- Place the jets in their housings in the crankcase and secure them using the bolts.
- Place the thrust washers in their seats on the third main bearing.
- The main journal half-bearings fitted on the crankshaft have been selected for their optimum fitting clearance.
The crankshaft supplied by the Parts Dept. comes without half-bearings and the main journals and crankpins are the "normal" size; the half-bearings to be fitted must therefore be selected identifying the class of each main journal and crankpin for the new crankshaft.
The following must be determined for the selection of main journal half-bearings:
- the numerical code stamped on the flywheel;
- the paint mark, if present, next to the main journals.
Below is an example of the identification of main journal grades.
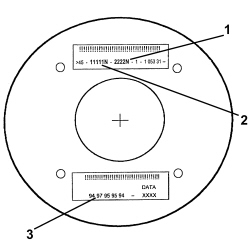
1 - Crankpin identification numerical code: the left number refers to the first timing side bearing; the final "N" is an insignificant code for 4 cylinder engines.
2 - Main journal identification numerical code: the first number refers to the first timing side bearing; the final "N" is an insignificant code for 4 cylinder engines.
3 - Series of numbers (if present), in groups of two digits, which indicate the dimensions (thousandth part) of the main journals: the first two numbers on the left refer to the first timing side bearing.
Only use the codes that relate to the key, all other codes on the flywheel should not be used.
- For the identification of the main journal grade, refer to the numerical code for reference 2 in the key.
- In the case of the example, the numbers 11111N indicate that all five bearings are Grade A (red) as indicated below.
- A further method for identifying the grade of the bearings is to read reference 3 (if present) in the diagram.
In the case of the example, the number 94 (first on the left) corresponds to the dimensions 52.994 for the first timing side bearing which identifies Grade A (red); the same method should be applied for other groups of two digits for the same reference 3 (97 - 95 - 95 - 94).
MAIN JOURNAL IDENTIFICATION
- Main journal grade A (normal), diameter 59.994 - 60.000 mm, RED paint mark, numerical code 1 (94 00)*
- Main journal grade B (normal), diameter 59.987 - 59.993 mm, BLUE paint mark, numerical code 2 (87 93)*
- Main journal grade C (normal), diameter 59.982 - 59.986 mm, YELLOW paint mark, numerical code 3 (82 86)*
- Main journal grade D (0.127 mm undersize), diameter 59.867 - 59.873 mm, BROWN paint mark, numerical code 6 (67 73)*
- Main journal grade E (0.127 mm undersize), diameter 59.860 - 59.866 mm, GREEN paint mark, numerical code 7 (60 66)*
- Main journal grade F (0.127 mm undersize), diameter 59.855 - 59.859 mm, BLACK paint mark, numerical code 8 (55 59)*
- (*): Last two numbers (thousandth part) of the main journal dimensions.
- In the case of the usage of a crankshaft where the maximum undersize for the bearings is 0.127 mm through grindings, the grade should be selected through the measurement of the diameter of the bearing using the above as a reference.
- Having defined the grade and the colour of each new or reground crankshaft bearings, it is necessary to select the thickness of the bearings that should be the same colour as the corresponding bearing; the pair of half-bearings required can be ordered from the Parts Dept. by quoting the order no.
- The above is designed to guarantee the optimum operational clearances for all the bearings.
Lastly, we wish to point out that, generally, the clearance between the main journal and the half-bearing, obtained through the selection method indicated above, should be within the following values:
- Minimum: 0.025 mm - Maximum: 0.052 mm; this value can be measured, as a final check, using the calibrated wire (Plastigage).
- Place the bearing caps complete with half-bearings in their seats.
The bearing caps have progressively numbered references (from zero to four starting from the front of the engine) which define the fitting position.
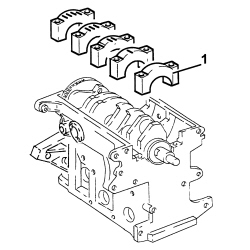
1. Tighten the bearing cap bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt | M12 | 2.4 ÷ 2.6 + 100° | 1.9 JTD 8V |
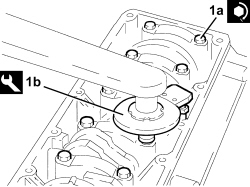
- Fit the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
- Rotate the crankcase through 90° on the overhaul stand.
- Rotate the crankshaft using the tool fitted previously until the cylinder concerned is at B.D.C.
- Refit the piston-connecting rod assemblies (1a) in their seats with upper connecting rod bearing halves using tool (1b).
For the selection of the connecting rod half-bearings, follow the procedure described previously for the main journal half-bearings.
The piston-connecting rod assemblies are fitted in the cylinder block/crankcase so that the combustion chamber in the piston is facing the intake side.
1. Test the crankpin clearance by applying plastigage to measure crankpin installation clearance.
- Place the crank pin caps complete with half-bearings in their seats.
Fit the connecting rods so that the number stamped on each rod faces toward the same side as the number stamped on the big end (inlet side).
1. Tighten the bolts (1a) to torque, using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
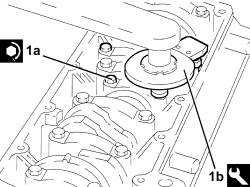
- Undo the nuts and remove the bearing caps tightened previously.
- Check that the thickness of the connecting rod half-bearings is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin half-bearings - Category A (red) | 1.527 - 1.531 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin half-bearings - Category B (light blue) | 1.530 - 1.534 mm | 1.9 JTD 8V |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin half-bearings - Category C (yellow) | 1.533 - 1.537 mm | 1.9 JTD 8V |
1. Use an appropriate graduated measuring tool (1a) to measure the clearance indicated by the plastigage (1b).
| Measurement | Value | Validity |
|---|---|---|
| Clearance between crankpins - crankshaft bearings | 0.030 - 0.056 mm | 1.9 JTD 8V 1.9 JTD 16V |
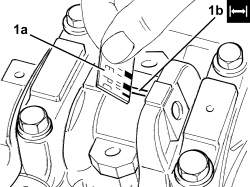
- If the value measured is not within the recommended figures, replace the connecting rod bearings.
- Carry out this test on all the crankpins, one at a time, without ever turning the crankshaft.
- Fit the connecting rod cap complete with half-bearing and secure it without tightening the bolts.
Fit the connecting rods so that the number stamped on each rod faces toward the same side as the number stamped on the big end (inlet side).
- Tighten the connecting rod cap bolts to the recommended torque using the angular tightening tool.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt | M9 | 2.4 ÷ 2.6 + 60° | 1.9 JTD 8V 1.9 JTD 16V |
- Remove the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820618000 | Flange | Crankshaft rotation | 1.9 JTD 8V 1.9 JTD 16V |
- Place the crankcase rear cover with built in oil seal in its housing.
- Tighten the crankcase rear cover bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Flywheel side oil seal cover | Bolt (pretreated to be replaced) | M6 | (engine crankcase side) 0.8 - 1.0 | 1.9 JTD 8V 1.9 JTD 16V 2.4 JTD 20V |
- Undo the cover and replace the oil filter cartridge.
- Place the engine oil filter mounting complete with heat exchanger in position and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Water/engine oil heat exchanger support | Bolt | M10 | 4.5 ÷ 5.5 | 1.9 JTD 8V |
- Fit the front crankcase cover with built-in oil pump complete with intake chamber and secure by tightening bolts to the specified torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Crankshaft oil seal front cover | Bolt (pretreated to be replaced) | M6 x 1 x 22 | 0.8 ÷ 1.0 | 1.9 JTD 8V |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Crankshaft oil seal front cover | Bolt | M6 x 1 x 35 | 0.8 ÷ 1.0 | 1.9 JTD 8V |
- Place the seal in its housing on the oil pump using the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860816000 | Fitting tool | Fitting oil pump seal | 1.9 JTD 8V |
- Position the toothed timing drive pulley in its housing and tighten the bolt (left hand thread) to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Toothed drive pulley | Left hand bolt | M16 | (crankshaft side) 32.3 - 35.7 | 1.9 JTD 8V 1.9 JTD 16V |
- Place the mounting complete with timing belt moving tensioner back in its housing and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing tensioner moving support | Bolt | M12 | 2.8 ÷ 3.1 + 40° +/- 2° | 1.9 JTD 8V |
- Clean the residues of sealant from the mating surfaces between the engine block and the crankcase sump.
- Apply a strip of silicone sealant to the contact surfaces between the crankcase sump and the engine block.
The sealant strip must be unbroken.
- Place the oil sump back in its housing.
When fitting the crankcase sump, take care not to damage the sealant strip.
Finish the installation operation within 10 minutes of applying the sealant.
- Tighten the side bolts fixing the crankcase sump.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump | Bolt | M8 | (engine crankcase side) 2.3 - 2.8 | 1.9 JTD 8V 1.9 JTD 16V |
- Tighten the bolts securing the sump to the crankcase, camshaft side and gearbox side, to the specified torque with the tool.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump | Bolt | M6 | (front and rear cover side) 0.8 - 1.0 | 1.9 JTD 8V 1.9 JTD 16V |
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860833000 | Spanner | Loosen/tighten the timing side and gearbox side bolts securing the crankcase sump | 1.9 JTD 8V 2.4 JTD 20V |
- Rotate the engine through 180° on the overhaul stand.
- Place the air conditioning compressor complee with mounting back in its housing and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| COMPRESSOR MOUNTING | Bolt | M10x1.25x75 | 4.5 ÷ 5.5 | 1.9 JTD 8V 1.9 JTD 16V |
1. Measure the piston projection in two places at 180° on the gudgeon pin axis using the tool and take the average of the two values measured for each piston.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1820253000 | Dial gauge support | Measure the piston projection/valve recess in relation to the cylinder head plane | 1.9 JTD 8V |
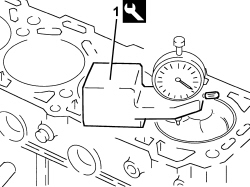
- Select the correct size cylinder head gasket depending on the maximum value between of the averages of the projection for each individual piston.
| Measurement | Value | Validity | ||
|---|---|---|---|---|
| Cylinder head gasket size with average maximum piston projection | projection 0.014 - 0.104 mm thickness (no reference) 0.770 - 0.870 mm | |||
| Measurement | Value | Validity | ||
|---|---|---|---|---|
| Cylinder head gasket size with average maximum piston projection | projection 0.105 - 0.205 mm thickness (one reference) 0.870 - 0.970 mm | |||
| Measurement | Value | Validity | ||
|---|---|---|---|---|
| Cylinder head gasket size with average maximum piston projection | projection 0.206 - 0.294 mm thickness (two references) 0.970 - 1.070 mm | |||
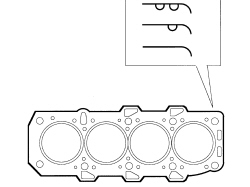
- Place the cylinder head centering bushes on the cylinder block.
- Place the cylinder head gasket selected in position.
The cylinder head gasket is ASTADUR type. The material from which the gasket is made undergoes a polymerization process during the operation of the engine so that it becomes considerably harder during usage. In order for the polymerization process to take place, it is necessary to:
- keep the gasket sealed in its casing until it is fitted;
- not lubricate the gasket or the contact surfaces with oil.
- Position the cylinder head on the cylinder block/crankcase.
1. Tighten the cylinder head bolts (1a) to the recommended torque using the angular tightening tool (1b).
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cylinder head | Bolt | M12 | (engine crankcase side) 6.2 - 6.8 + 90° + 90° + 90° | 1.9 JTD 8V |
Achieve the figure of 6.5 daNm by a pretightening of 2.0 daNm subsequently increased by a torque of 4.5 daNm to achieve a nominal value of 6.5 daNm
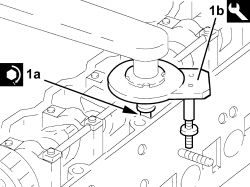
Follow the order shown in the figure for each tightening sequence.
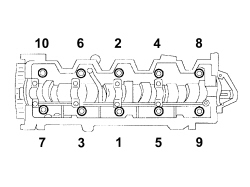
- Place the tappet cover complete with gasket back in its housing and secure it by tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Tappet cover | Bolt | M6 | (cylinder head side) 0.8 - 1.0 | 1.9 JTD 8V |
- Place the pressure pump mounting complete with alternator back in its housing and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pressure pump mounting | Bolt (pretreated to be replaced) | M8 | 2.3 ÷ 2.8 | 1.9 JTD 8V |
- Place the pipe from the pressure pump to the fuel return manifold pipe back in its housing and secure it using the bands.
- Place the new rigid pipe between the pump and the fuel manifold back in its housing and secure it tightening the connectors to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipe from pressure pump to fuel manifold | Connector | M14 | (fuel manifold side) 2.2 - 2.4 | 1.9 JTD 8V 1.9 JTD 16V 2.4 JTD 20V |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Pipe from pressure pump to fuel manifold | Connector | M12 | (pressure pump side) 2.2 - 2.4 | 1.9 JTD 8V 1.9 JTD 16V 2.4 JTD 20V |
1. Undo the bolt fixing the crankcase front cover shown in the diagram.
- Temporarily fit the toothed timing drive belt on the toothed drive pulley.
2. Fit the tool.
The crankshaft must be rotated, using small movements, to allow the locating dowel on the timing drive pulley to be inserted in the opening in the tool.
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000003000 | Template | Engine tuning | 1.9 JTD 8V 1.9 JTD 16V 2.4 JTD 20V |
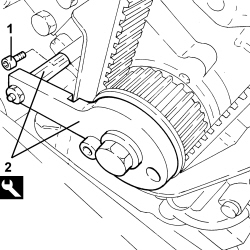
1. Rotate the driven toothed pulley until the timing references are aligned.
2. Fully fit the toothed timing drive belt.
3. Use a screwdriver for leverage on the tensioner arm until the reference (3a) for the tensioner is in the maximum tension position and tighten the tensioner bolt (3b) to the recommended torque in this position.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing moving tensioner | Nut | M8 | 2.3 ÷ 2.8 | 1.9 JTD 8V 1.9 JTD 16V |
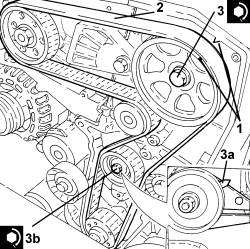
- Remove the timing tool.
- Rotate the crankshaft through two revolutions.
1. Loosen the moving timing tensioner nut.
2. Use a screwdriver for leverage on the tensioner arm until the reference (2a) for the tensioner is in line with the reference opening (2b) and tighten the tensioner bolt (2c) to the recommended torque in this position.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing moving tensioner | Nut | M8 | 2.3 ÷ 2.8 | 1.9 JTD 8V 1.9 JTD 16V |
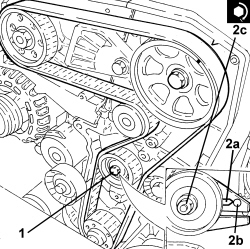
- Rotate the crankshaft through two revolutions and check that the reference for the tensioner remains in line with the reference opening.
- Check the correct timing again, refitting the timing tools and checking the timing references are aligned.
- If not, repeat the tensioning/timing procedure.
- Tighten the bolt fixing the crankcase front cover removed previously.
- Fit the power unit rigid support and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing side power unit rigid support | Bolt | M10 | (engine crankcase side) 4.5 - 5.5 | 1.9 JTD 8V 1.9 JTD 16V |
- Position the auxiliary drivebelt fixed tensioner in its housing and secure it tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine components single belt fixed tensioner | Bolt | M8 | 2.2 ÷ 2.7 | 1.9 JTD 8V |
- Position the crankshaft pulley in its housing and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Services pulley on crankshaft | Bolt | M8 | (drive pulley side) 2.3 - 2.8 | 1.9 JTD 8V 1.9 JTD 16V |
- Place the engine components single belt in its housing using a spanner on the moving tensioner.
- Place the exhaust manifold gasket in its housing.
- Place the exhaust manifold - turbocharger assembly complete with precatalyzer back in its housing and secure it tightening the nuts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Turbocharger and exhaust manifold assembly | Nut | M8 | (cylinder head side) 2.2 - 2.7 | 1.9 JTD 8V |
- Connect the engine oil return hose from the turbocharger to the crankcase and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil supply pipe from turbocharger | Bolt | M8 | (engine crankcase side) 2.2 - 2.7 | 1.9 JTD 8V 1.9 JTD 16V |
- Connect the engine oil turbocharger supply pipe to the crankcase and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil supply pipe to turbocharger - crankcase side | Connector | M12 | 2.2 ÷ 2.7 | 1.9 JTD 8V |
- Connect the E.G.R. exhaust gas intake hose to the exhaust manifold and secure it using the bolts.
- Place the oil dipstick pipe back in its housing and fasten it to the oil sump using the bolt.
- Place the water pump rigid return in position and secure it using the bolts.
- Connect the hose to the rigid pipe and securing it using the band.
- Place the timing belt side guard in its housings and secure it using the bolts.
- Fit the timing belt protective cover and secure it using the bolts.
- Place the support complete with vacuum reservoir in position, seucre it using the bolts and connect the two pipes.
- Place the duplex pipes in position and connect them to the water-oil heat exchanger.
- Connect the heater coolant supply and return pipes to the thermostat.
- Refit the electrical wiring
- Connect the electrical connection for the fuel pressure sensor.
- Connect the electrical connection for the throttle casing.
- Connect the electrical connection for the coolant temperature sensor.
- Connect the electrical connection for the excess pressure sensor.
- Connect the electrical connection for the E.G.R. solenoid valve.
- Connect the electrical connections for the injectors.
- Connect the electrical connection for the fuel pressure regulator.
- Connect the glow plug electrical connections.
- Connect the electrical connection for the engine oil level sensor.
- Connect the electrical connection for the rpm sensor.
- Connect the electrical connections for the alternator.
- Connect the electrical connection for the minimum engine oil pressure switch.
- Connect the electrical connection for the air conditioning compressor engagement solenoid.
Op. 1004D40 ENGINE - POSITION ON STAND AND REMOVE
Removing
1. Remove the toothed drive pulley
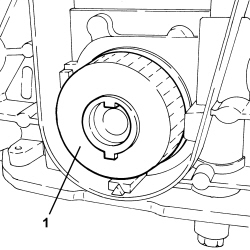
1. Undo the bolts (1a) and remove the alternator (1b).
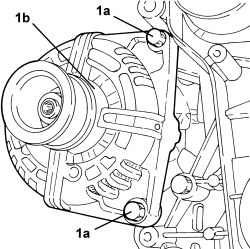
1. Undo the bolt (1a) and remove the detonation sensor (1b).
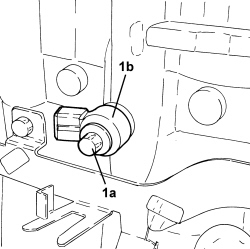
1. Undo the bolt (1a) and remove the rpm sensor (1b).
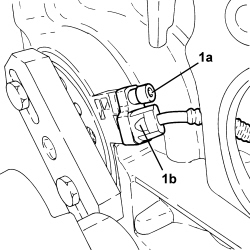
- Undo the bolts and remove the connector holder bracket.
1. Undo the bolts (1a) and remove the engine oil filter mounting (1b) complete with heat exchanger.
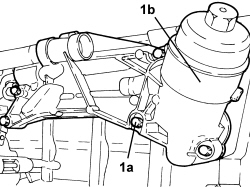
- Place the engine oil filter mounting complete with heat exchanger in a vice fitted with protective jaws.
1. Undo the bolts and remove the water-oil heat exchanger (1a) from the engine oil filter mounting (1b).
- Remove the gaskets.
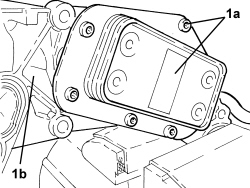
1. Undo the plug (1a) and remove the oil filter cartridge (1b).
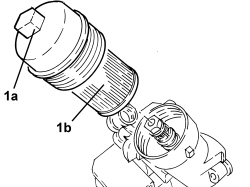
1. Undo the bolts (1a) and remove the rigid return pipe (1b) to the water pump complete with O-ring.
2. Undo the bolts (2a) and remove the air conditioner compressor (2b).
3. Undo and remove the engine oil pressure warning light switch.
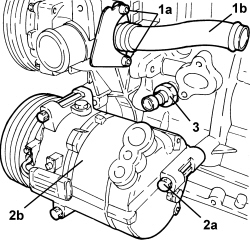
1. Undo the bolt (1a) and remove moving tensioner (1b).
2. Undo the bolt (2a) and remove fixed tensioner (2b).
3. Undo the bolts (3a) and remove the crankshaft oil seal front cover (3b).
- Remove the gasket.
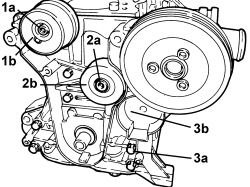
- Place the crankshaft oil seal cover assembly in a vice fitted with protective jaws.
1. Undo the bolts (1a) and remove the water pump pulley (1b).
2. Undo the bolts (2a) and remove the cover (2b) complete with water pump impeller.
- Remove the gasket from the water pump cover.
- Remove the centering pins.
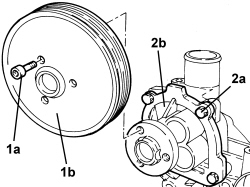
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
- Rotate the crankshaft using the tool fitted previously until the piston concerned is at B.D.C.
- Mark the connecting rod cap and the connecting rod to be removed.
1. Undo the bolts (1a) and remove the connecting rod caps (1b) and lower half-bearings.
2. Remove the pistons complete with connecting rods and upper half-bearings.
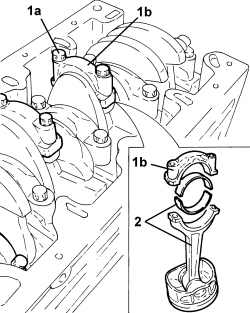
The arrow (a) on the piston crown facing the timing side indicates the fitting direction. The connecting rod-cap matching is the "BREAK" with a compulsory position. The projection (b) on the connecting rod and the cap should be facing the flywheel with the arrow on the crown pointing towards the timing side to ensure the correct piston-connecting rod matching.
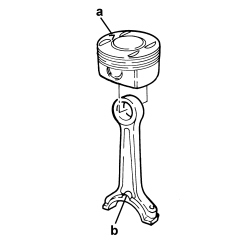
Op. 1028H54 PISTON WITH CONNECTING ROD - DISMANTLING AT THE BENCH
- Release the rpm sensor support ring and remove it.
- Remove the crankshaft rear seal.
- Check that the crankshaft endfloat is within specified limits.
| Measurement | Value | Validity |
|---|---|---|
| Crankshaft endfloat (mm) | 0.100 ÷ 0.202 | 1.8 |
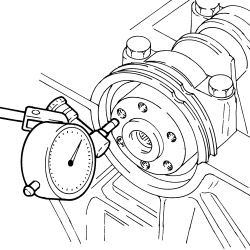
- If the value is not within the recommended limits, replace the half-bearings for main journal 3 and repeat the checking operation.
| Measurement | Value | Validity |
|---|---|---|
| Main journal 3 width (mm) | 26.000 ÷ 26.052 | 1.8 |
1. Undo the bolts (1a) and remove the main journal caps (1b) and lower half-bearings.
The bearing caps are numbered from 1 to 5 starting from the timing side.
2. Remove the crankshaft from the cylinder block/crankcase.
3. Remove the upper main journal half-bearings.
4. Remove the thrust washers from the centre support.
5. Undo the bolts (5a) and remove the engine oil jets (5b).
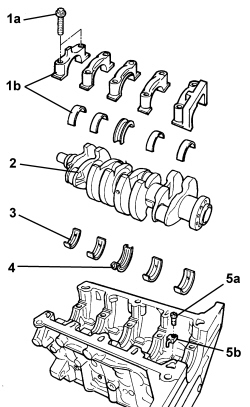
1. Place the crankshaft in the cylinder block/crankcase on the supports and check that the radial clearance is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Crankshaft eccentricity (mm) | 0.03 | 1.8 |
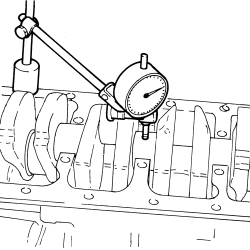
- Remove the crankshaft from the cylinder block/crankcase.
Op. 1020A46 CRANKCASE OIL SUMP PARTITION - R.R. WITH CRANKCASE SUMP REMOVED
Op. 1084A40 ENGINE OIL LEVEL SENSOR - R + R
- Drill and remove the water/oil sealing plugs from the crankcase to allow for washing the ducts.
Refitting
- Clean the residues of sealant from the mating surfaces between the cylinder head and the engine block.
- Clean the residues of sealant from the mating surfaces between the oil sump and the engine block.
- Clean the parts removed thoroughly and check their condition visually.
- Fit the water/oil sealing plugs in the engine block using suitable fitting tools.
- Place the engine oil jets in their housings and tighten the bolts.
- Lubricate all the mechanical components with engine oil.
- Check that the cylinder head support surface does not have cracks or grooves.
1. Using a calibrated metal rule and a feeler gauge, check the flexible yield, widthwise and lengthwise and the diagonal defromation of the upper engine block surface.
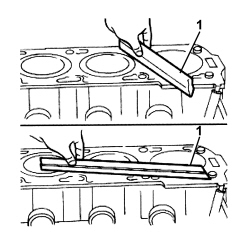
1. The following information is stamped on the engine block: production date (1a), cylinder liner/bore grade (1b), main journal bearing grade (1c).
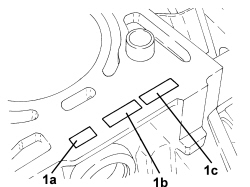
1. Measure the inner diameter of the cylinder bores as illustrated in the diagram below using a gauge for the interior.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade 00 (mm) | 80.492 ÷ 80.508 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner inner diameter - Grade 05 (mm) | 80.542 ÷ 80.558 | 1.8 |
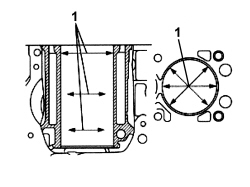
- If the cylinder bore internal diameter is not within the recommended limit, ream the cylinder bores following the recommended oversizes.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder liner bore diameter oversize (mm) | 0.5 | 1.8 |
In the case of reaming, all the cylinder bores must have the same oversize.
After reaming the original code must be invalidated and the new oversize code stamped on the engine block.
- Check that the diameter of the main journals corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter (brown) | 54.980 ÷ 54.997 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter (green) | 54.980 ÷ 54.997 | 1.8 |
- If the diameter of the main journals is not correct, they should be reground to the recommended undersizes.
| Measurement | Value | Validity |
|---|---|---|
| Main journal diameter undersize (mm) | 0.25/0.50 | 1.8 |
- Check that the diameter of the crankpins corresponds to the recommended figures.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter (mm) | 42.971 ÷ 42.987 | 1.8 |
- If the diameter of the crankpins is not correct, they should be reground to the recommended undersizes.
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter undersize (blue) (mm) | 0.25 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Crankpin diameter undersize (white) (mm) | 0.50 | 1.8 |
- Check that the length of main journal "3" (guide bearing) is within the recommended values.
| Measurement | Value | Validity |
|---|---|---|
| Main journal 3 width (mm) | 26.000 ÷ 26.052 | 1.8 |
- If the diameter of the main journal 3 is not correct, it should be reground to the recommended undersizes.
| Measurement | Value | Validity |
|---|---|---|
| Main journal 3 width undersize (mm) | 0.20/0.40 | 1.8 |
- Check the crankshaft and connecting rod bearings bearing in mind that no adjustment operations should be carried out on the half-bearings. Replace them if scoring or signs of binding are noted.
- Fit the upper half-bearings on the engine block making sure that they are perfectly clean and have been lubricated with engine oil.
If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
- Fit the crankshaft into its seat on the crankcase.
1. Fit the calibrated wire (plastigage) for measuring the bearing clearance.
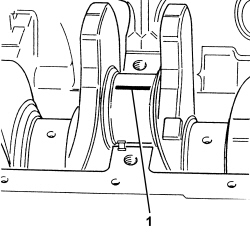
- Fit the lower half-bearings on the connecting rod caps making sure that they are perfectly clean and have been lubricated with engine oil.
If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
- Fit the bearing caps following the fitting position marked on them and tighten the bolts to the recommended torque.
The fixing bolts removed previously can be reused just to check the bearing clearance.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt (to be replaced) | 5.0 + 45° + 15° | 1.8 |
1. Remove the bearing caps fitted previously and, using a suitable graduated measuring instrument (1a), measure the clearance shown by the calibrated wire (1b).
Check the clearance for all the main journals taking care to do it one bearing at a time without ever moving the crankshaft.
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main bearings - crankshaft bearings (mm) | 0.005 ÷ 0.059 | 1.8 |
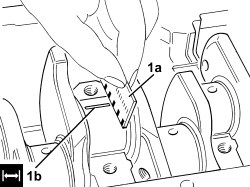
- If the values are not within the recommended limits, replace the half-bearings and repeat the operation of checking the clearance.
- The size of the main journal half-bearings is given.
| Measurement | Value | Validity |
|---|---|---|
| Main half bearing nominal thickness (brown) (mm) | 1.987 ÷ 1.993 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.25) (brown/blue) (mm) | 2.112 ÷ 2.118 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.50) (brown/white) (mm) | 2.237 ÷ 2.243 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Main half bearing nominal thickness (green) (mm) | 1.993 ÷ 1.999 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.25) (green/blue) (mm) | 2.118 ÷ 2.124 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.50) (green/white) (mm) | 2.243 ÷ 2.249 | 1.8 |
- Apply adhesive putty in the side splining of main journal cap number 5 (flywheel side) and place it in position.
- Fit the remaining main journal caps following the position marked on them.
- Tighten the new connecting rod cap fixing bolts to the specified torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bearing caps | Bolt (to be replaced) | 5.0 + 45° + 15° | 1.8 |
- Clean any carbon residues carefully from the pistons.
- Check that the outer diameter of the pistons perpendicular to the gudgeon pin axis 14.5 mm from the lower edge is within the recommended values.
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - Grade 00 (mm) | 80.455 ÷ 80.465 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter - Grade 05 (mm) | 80.505 ÷ 80.515 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Piston outer diameter oversize (mm) | 0.5 | 1.8 |
- If these values do not correspond to the recommended figures, replace the piston complete with piston rings and gudgeon pin.
- The clearance between the piston and the liner/bore is given below.
| Measurement | Value | Validity |
|---|---|---|
| Clearance between piston - cylinder liner/bore (mm) | 0.045 ÷ 0.175 | 1.8 |
- Check that the outer diameter of the gudgeon pin corresponds to the recommended figures; if not, replace the piston complete with piston rings and gudgeon pin.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin outer diameter (mm) | 19.000 | 1.8 |
- Check that the clearance between the gudgeon pin and the housings in the connecting rod and piston are within the recommended values.
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin - connecting rod clearance (mm) | 0.015 ÷ 0.021 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Gudgeon pin - piston clearance (mm) | 0.02 ÷ 0.06 | 1.8 |
- Check that the thickness of the piston rings is within the recommended limits.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring thickness (mm) | 1.170 ÷ 1.190 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring thickness (mm) | 1.170 ÷ 1.190 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring size (mm) | 1.90 ÷ 1.98 | 1.8 |
- Fit the piston rings in the cylinder bore and, using a feeler guage, check that the gap between the two ends is within the recommended values, or else they must be replaced.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring gap (mm) | 0.20 ÷ 0.40 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring gap (mm) | 0.40 ÷ 0.60 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Piston oil scraper ring gap (mm) | 0.25 ÷ 0.75 | 1.8 |
1. Check that the backlash (1a) between the circlips (1b) and the housing in the piston (1c) corresponds to the recommeded figure; if this is not the case, replace the circlips.
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 1st piston ring endfloat (mm) | 0.04 ÷ 0.08 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Cylinder compression 2nd piston ring endfloat (mm) | 0.03 ÷ 0.07 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Oil scraper ring endfloat (mm) | 0.20 ÷ 0.35 | 1.8 |
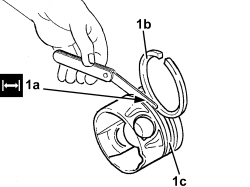
Op. 1028H54 PISTON WITH CONNECTING ROD - DISMANTLING AT THE BENCH
1. Fit the piston complete with connecting rod (1a) and half-bearings using the tool (1b) for compressing the circlips and then fitting them in the cylinder liner/bore.
2. Position the piston with the arrow (2a) facing the timing side and the projection (2b) facing the flywheel.
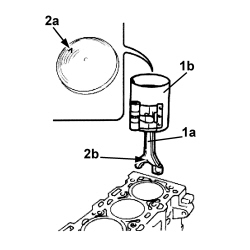
1. Fit the calibrated wire (plastigage) for measuring the bearing clearance.
2. Fit the lower connecting rod half-bearings on the caps making sure that they are perfectly clean and have been lubricated with engine oil.
If the crankshaft has been ground, fit new oversize half-bearings to restore the initial tolerance conditions.
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing nominal thickness (mm) | 1.485 ÷ 1.497 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.25) (blue) (mm) | 1.610 ÷ 1.622 | 1.8 |
| Measurement | Value | Validity |
|---|---|---|
| Connecting rod half-bearing thickness oversize (0.50) (white) (mm) | 1.735 ÷ 1.747 | 1.8 |
3. Fit the connecting rod caps matching them with the connecting rod using the references made during the dismantling and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt (to be replaced) | 2.5 + 30° + 15° | 1.8 |
The fixing bolts removed previously can be used just to check the bearing clearance.
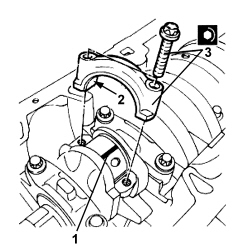
1. Undo the bolts and remove the bearing caps fitted previously and, using a suitable graduated measuring instrument (1a), measure the clearance shown by the calibrated wire (1b).
| Measurement | Value | Validity |
|---|---|---|
| Clearance between main ljournals - crankshaft bearings (mm) | 0.019 ÷ 0.071 | 1.8 |
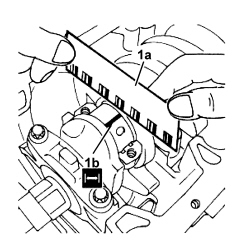
If the values are not within the recommended limits, replace the half-bearings and repeat the operation of checking the clearance.
- Fit the connecting rod caps and secure them by tightening the fixing bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Connecting rod big end bearing caps | Bolt (to be replaced) | 2.5 + 30° + 15° | 1.8 |
- Remove the tool for rotating the crankshaft.
1. Place a new flywheel side oil seal (1a) in the housing using the tool (1b).
| Tool | Description | Function | Validity |
|---|---|---|---|
| 1860843000 | Fitting tool | Fitting crankshaft rear oil seal | 1.8 |
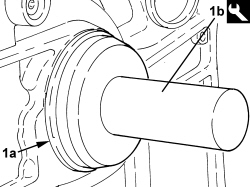
- Fit the rpm sensor support seal on the oil seal fitted previously.
- Position the rpm sensor in its housing and secure it to the support seal using the bolt.
Op. 1084B18 ENGINE OIL PUMP, REMOVED - CHECK AT BENCH
- Place the crankshaft oil seal front cover in a vice fitted with protective jaws.
- Fith the water pump cover with a new gasket and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Water pump | Bolt | 0.8 | 1.8 |
- Position the water pump pulley in its housing and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Water pump pulley | Bolt | 2.0 | 1.8 |
- Fit the crankshaft oil seal front cover centering bushes on the crankcase.
- Fit a new crankshaft oil seal front cover gasket.
- Place the crankshaft front oil seal cover in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Crankshaft oil seal front cover | Bolt | 2.0 | 1.8 |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| AIR CONDITIONING COMPRESSOR | Bolt | 2.25 ÷ 2.75 | 1.8 16v |
- Place the engine oil pressure switch in position and tighten it to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Switch for engine oil pressure warning light | 2.0 | 1.8 |
- Place the water pump rigid return pipe, complete with new gasket, in position and tighten the bolts.
- Place the oil filter mounting in a vice fitted with protective jaws and replace the gaskets.
- Place the water-oil heat exchanger in position on the engine oil filter mounting and secure it using the bolts.
- Place a new oil filter cartridge in position and tighten the cover to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil filter cover | 2.5 | 1.8 |
- Remove the engine oil filter mounting assembly from the vice, place it in position on the left side of the crankcase and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil filter and heat exchanger mounting | Bolt | 2.5 | 1.8 |
- Position the detonation sensor in its housing and secure it tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Detonation sensor | Bolt | M8 | 1.5 ÷ 2.5 | 1.8 |
- Place the connector holder bracket in position and fit the rpm sensor connector.
- Place the alternator in position and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Alternator | Bolt | M10 | 4.5 ÷ 5.5 | 1.8 16v 2.4 JTD 20v |
- Place the toothed drive pulley in its housing on the crankshaft.
- Apply a bead of silicon sealant about 2 mm thick to the contact areas between the engine block, 5th main bearing cap (flywheel side) and the crankshaft oil seal front cover.
1. Apply a bead of silicon sealant about 3 mm thick to the edge of the sump and around the oil recirculation and inlet connectors as illustrated.
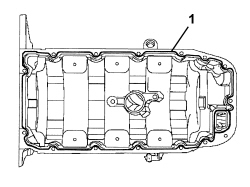
- Refit the oil sump in its seat and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump - crankcase side | Bolt | 1.0 | 1.8 |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine oil sump - gearbox side | Bolt | 4.0 | 1.8 |
- Rotate the overhaul stand through 180 °.
- Fit the locating bushes for the engine block.
- Fit a new cylinder head gasket.
- Place the cylinder head in position and tighten the fixing bolts to the recommended torque, following the order illustrated in the diagram.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Cylinder head | Bolt (to be replaced) | 2.5 + 90° + 90° + 90° + 45° | 1.8 |
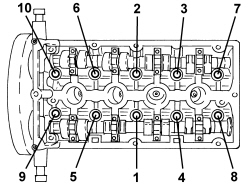
1. Fit the tool (1a) in the special splining on the camshafts (1b).
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000012000 | Template | Camshaft timing | 1.8 |
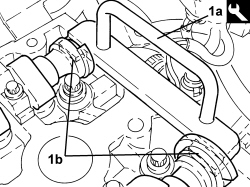
1. Fit the tool (1a) on the toothed driven pullies (1b).
| Tool | Description | Function | Validity |
|---|---|---|---|
| 2000012100 | Template | Camshaft timing | 1.8 |
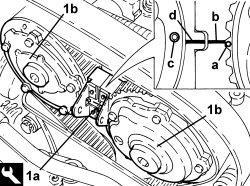
Fit the inlet side template first and then the exhaust side one.
When the templates have been fitted, check that:
- the reference (a) on the exhaust side pulley is aligned with the reference (b) on the corresponding timing template;
- the pin (c) on the inlet side pulley is in the position illustrated, in relation to the reference (d) on the corresponding timing template.
- Using the special tool, rotate the crankshaft and place the reference on the toothed drive pulley in line with the reference (triangle) on the crankshaft oil seal front cover.
- Using a spanner, rotate the timing belt moving tensioner in a clockwise direction until the tensioner locking pin can be placed inside the opening.
- Fit a new timing belt in place, taking care not to move the crankshaft timing references.
1. Check the crankshaft timing by checking that the references illustrated in the diagram are aligned.
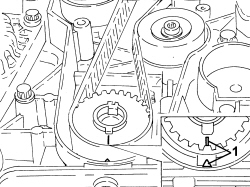
- Fit the timing belt definitively adjusting the moving tensioner to remove the locking pin.
- Remove the templates used for timing the camshafts.
- Place the cam cover in position and secure it by tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Tappet cover | Bolt | 0.8 | 1.8 |
- Place the ignition coil module in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Ignition coil module | Bolt | M6 | 0.6 ÷ 1.0 | 1.8 |
- Place the ignition coil cover in its housing and secure it using the retaining clips.
- Fit the timing belt lower protective cover and secure it using the bolts.
- Place the auxiliary belt pulley and washer in position and tighten the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Services pulley on crankshaft | Bolt (to be replaced) | 9.5 + 30° + 15° | 1.8 |
Prevent the crankshaft from rotating using the flange fitted previously on the crankshaft.
Check that the timing reference on the auxiliary drive pulley is aligned with the reference on the timing belt lower protective cover.
- Place the water pump rigid rear return pipe, complete with new seals in position and secure it to the thermostat tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Rigid pipe on thermostat | Bolt | 0.8 | 1.8 |
- Fit the new exhaust manifold gasket on the cylinder head studs.
- Place the exhaust manifold - catalytic converter in its housing with the mounting bracket on the crankcase and tighten the fastenings to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Exhaust manifold with catalytic converter | Nut (to replace) | (cylinder head side) 2.0 | 1.8 2.2 |
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Bracket side caztalyzer | Bolt | 2.0 | 1.8 |
- Place the exhaust pipe heat shield in its housing and secure it using the bolts.
- Place the oil dipstick pipe back in its housing and fasten it to the cylinder head using the bolt.
- Place the modular intake chamber in its housing and secure it to the cylinder head tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Modular intake manifold | Bolt | 2.0 | 1.8 |
- Place the injection control unit in its housing on the modular intake chamber and tighten the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Injection/ignition system control unit | Bolt | M6 | 0.8 ÷ 1.0 | 1.8 |
- Place the throttle body in position and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Throttle body built into DVL | Bolt | M6 | 0.8 ÷ 1.0 | 1.8 |
- Connect the water supply and return pipes to the throttle body and secure them using the bands.
- Connect the corrugated oil vapour hose to the tappet cover and to the throttle body and secure it using the retaining clips.
- Connect the rapid connector for the throttle body coolant supply pipe, thermostat mounting side.
- Place the wiring in its housing on the engine and secure it using the retaining clips.
- Connect the electrical connection for the injection control unit.
- Connect the electrical connections for the injectors.
- Connect the electrical connection for the phase transformer solenoid, inlet side.
- Connect the electrical connection for the fuel vapour flow enablement solenoid valve.
- Connect the electrical connection for the throttle casing.
- Connect the electrical connection for the modular intake manifold control actuator solenoid valve.
- Connect the electrical connection for the rpm sensor.
- Connect the electrical connection for the detonation sensor.
- Connect the electrical connection for the engine oil level sensor.
- Place the starter motor in its housing and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Starter motor | Bolt | 2.5 | 1.8 16v |
- Connect the earth lead to the cylinder head and secure it using the bolt.
- Connect the electrical connection of the ignition coil module.
- Connect the electrical connection for the water temperature sensor on the thermostat.
- Connect the electrical connection for the water temperature regulator on the thermostat.
- Connect the electrical connection for the inlet side timing sensor.
- Connect the electrical connection of the exhaust side timing sensor.
- Connect the electrical connection for the upper Lambda sensor and secure it to the mounting bracket.
- Fasten the wiring retaining duct to the tappet cover using the clips.
- Connect the electrical connection for the phase transformer solenoid, exhaust side.
- Connect the electrical connection for the minimum engine oil pressure switch.
- Connect the electrical connection for the air conditioning compressor.
- Place the intermediate timing belt protective cover in position.
- Fit the upper timing belt protective cover and secure it using the bolts.
- Place the power unit rigid support in position and secure it tightening the bolts to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Timing side power unit rigid support | Bolt | M10 | 5.0 ÷ 6.0 | 1.8 |
- Position the auxiliary drive belt moving tensioner in its housing and secure it tightening the bolt to the recommended torque.
| Component | Fastening | dia | Value (daNm) | Validity |
|---|---|---|---|---|
| Engine components single belt moving tensioner | Bolt | M10x1.5 | 5.0 | 1.8 1.9 JTD 16v 1.9 JTD 8v 2.4 JTD 20v |
- Adjust the moving tensioner with a wrench and fit the auxiliary drive belt.
Parts & tools for this job For 2005 Fiat Croma
- PARTEngine gasket setSearch: Fiat Croma 2005 engine gasket set
- TOOLTorque wrenchSearch: 3/8 inch torque wrench
- TOOLFeeler gauge setSearch: feeler gauge set
Links open Amazon search results in a new tab. As an Amazon Associate I earn from qualifying purchases.