
Crankshafts with Pluigs (page 3 of 4)
- Make
- Peugeot
- Model
- J5 Pocket Mechanic, 1.8 and 2.0 petrol
- Year
- 1987–1994
- Section
- Engine assembly
EngineCrankshafts with Pluigs · page 3 of 4
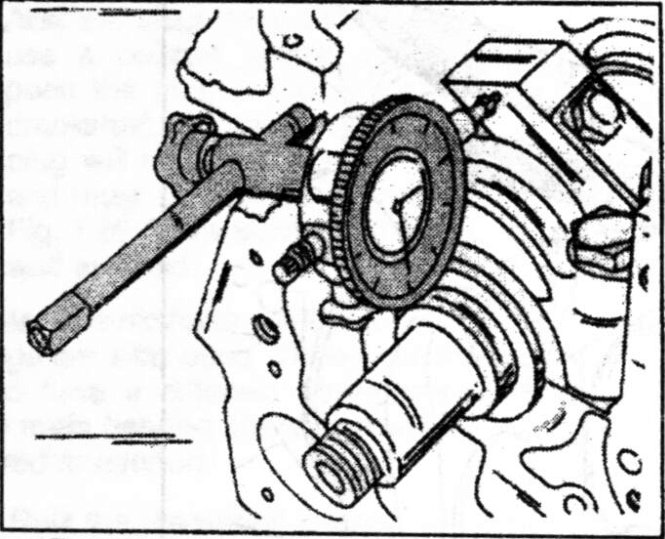
- Insert new rubber seals into the bearing cap and fit the tool shown in Fig. 1.32 to the cap. Insert the assembly into the cylinder block, taking care that the two side shims are pushing against the seals. Lubricate the shims and fit the whole assembly into the block. As the special tool shown is most probably not available, you can use thin sheet metal and insert them between the cylinder block and the side seals. Knock the bearing cap in position and remove the special tool (or the sheet metal pieces).
- Re-tighten the two bearing cap bolts evenly across to a torque of 7.5 kgm (54 ft.lb.).
- The side seals will protrude above the crankcase sealing face and must be cut-off. 2.0 mm of the seals must, however, remain. To obtain the exact length, use a piece of sheet metal of this thickness and drill a hole of the diameter of the seals into it. Place the sheet metal in position as shown in Fig. 1.33 and cut off the emerging ends. Both seals must be treated in this manner. The flat metal piece must have a thickness of exactly 2.0 mm.
- Thoroughly clean the flywheel face on the crankshaft and the flywheel itself and fit the flywheel to the crankshaft (only one position possible). Coat the flywheel bolts with “Loctite” and tighten them evenly to 6.75 kgm (49 ft.lb.). The crankshaft must be blocked against rotation in suitable manner.
- Insert the clutch driven plate into the flywheel and fit the clutch (refer to the relevant section). If the original parts are refitted, align the marks made during dismantling before tightening the clutch securing bolts. The bolts are tightened evenly to 1.5 kgm (11 ft.lb.).
- Fit the marked cylinder liners with the seals or steel shims into their marked bores. The identifications tabs must be arranged on opposite sides of the cylinder block, i.e. on one side for the fist cylinder and on the opposite side for the second cylinder.
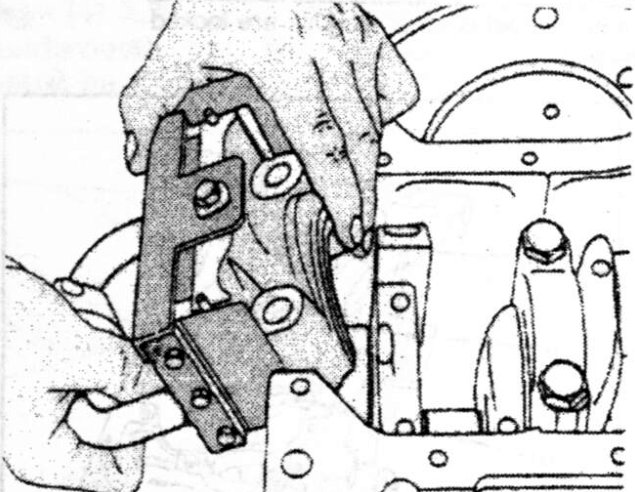
- The protrusion of the cylinder liners should now be measured with the
Parts & tools for this job For 1987 Peugeot J5
- PARTEngine gasket setSearch: Peugeot J5 1987 engine gasket set
- TOOLTorque wrenchSearch: 3/8 inch torque wrench
- TOOLFeeler gauge setSearch: feeler gauge set
Links open Amazon search results in a new tab. As an Amazon Associate I earn from qualifying purchases.